Profil pro extrudování 2020 má rozměry 20 mm × 20 mm a tento rozměr je jediné, co název určuje. Šířka drážky, tloušťka stěny, slitina a stav vytvrzení a tolerance řezu jsou ponechány na tom, kdo vystaví objednávku — a právě proto dva profily fakturované jako “2020” dorazí s drážkou, do které nepasují T-matice již uložené v zásuvce, nebo se stěnou přibližně o 20 % lehčí, než měl schválený vzorek.
O tom, zda se rám sestaví, rozhodují čtyři čísla:
- Šířka drážky — 6 mm, 5 mm nebo 6,35 mm. Název neříká která.
- Tloušťka stěny — důvod, proč se dva profily 20 mm mohou lišit hmotností o čtvrtinu.
- Slitina, stav vytvrzení a norma, podle níž se objednávka kontroluje — tři rozhodnutí obvykle stlačená do jednoho slova.
- Délka řezu a její tolerance — co odlišuje seznam řezů od požadavku.
Co “2020” specifikuje
Název je průřez, ne norma
První dvojice číslic udává šířku v milimetrech a druhá dvojice výšku, takže 2020 je 20 mm čtverečních, 2040 je 20 mm na 40 mm a 4040 je 40 mm čtverečních. V metrické řadě rámových profilů tato stupnice postupuje 2020 → 2040 → 4040 → 8080 a každý krok je geometrie.
Žádná publikovaná norma nedefinuje průřez “2020” — ani EN, ISO ani ASTM. EN 755-9 a EN 12020-2 popisují, jak se extrudovaný profil toleruje a měří; ani jedna neříká, jak široká má být drážka, jak silná má být stěna nebo kde mají být poloměry rohů. Ty pocházejí z matrice a ze systému příslušenství, k jehož spojování je průřez navržen.
Číslo se také kryje s označením slitiny. 2020 je registrovaná slitina Al-Cu-Li vyvinutá na konci 50. let 20. století pro konstrukce křídel letadel a samotné vyhledání tohoto termínu odhalí její vlastnosti. Nemá žádnou souvislost s profilem s T-drážkou 20 mm, který se obvykle lisuje z 6063.
Odkud pochází geometrie drážky
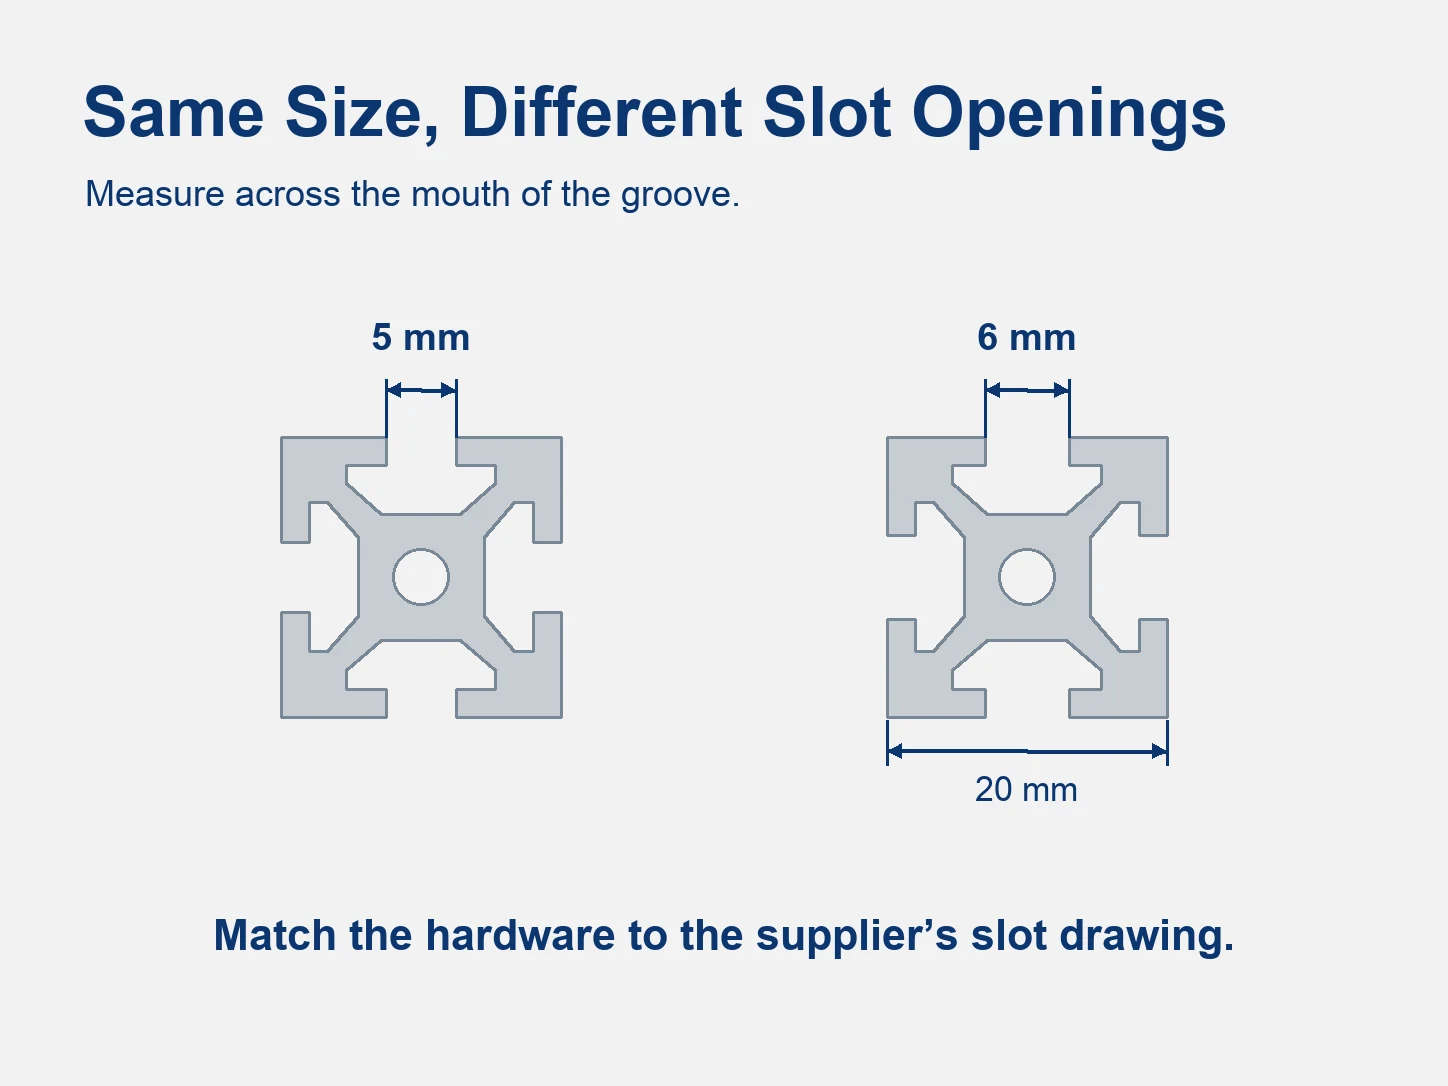
Profil 2020 se kupuje do systému a drážku vlastní systém. Metrická řada 20, ve které pracuje většina evropských a asijských výrobců strojů, má drážku 6 mm. Severoamerická řada 20 je postavena kolem drážky 1/4 in (6,35 mm). V některých řadách koluje také varianta 5 mm.
Důsledkem je, že drážka je pevně dána ještě před objednáním profilu — T-maticemi, konzolami a kolečky již specifikovanými v CAD modelu nebo ještě uloženými v zásuvce z poslední stavby. Příslušenství mezi systémy nepřechází a nabídka na “2020”, která neuvádí rozměr drážky, necituje díl, který byl navržen.
Rozměry a tolerance, které rozhodují o lícování
Tolerance průřezu
Průřez se řídí dvěma normami a výkres rozhoduje, která platí. EN 12020-2 pokrývá extrudované přesné profily z 6060 a 6063 s užšími pásmy. EN 755-9 pokrývá extrudované profily obecně se širšími pásmy.
Takže čelní plocha 20 mm nemá ve výchozím stavu jednu toleranci; pásmo, které dorazí, je pásmo, které objednávka uvedla. Toto pásmo se také sčítá. Tři profily naskládané na jeho vnější hranici posunou rohovou konzolu dále, než její vůle dovoluje, a spoj nakreslený jako tupý se uzavře s viditelným stupínkem.
Řešením je řádek na výkresu: uvést normu a uvést rozměr, na kterém záleží. U rámového profilu to obvykle bývá čelní plocha 20 mm a vzdálenost drážka–drážka, nikoli stěna.
Šířka drážky: 6 mm, 5 mm a imperiální čtvrt palce
| Řada drážky | Otvor | Hardware, který přijímá |
|---|---|---|
| Metrická řada 20 | 6 mm | T-matice M5 a vkládací matice; M4 u lehčích spojovacích dílů |
| Rozsah variant | 5 mm | M4 a menší; hardware 6 mm se neusadí |
| Severoamerická řada 20 | 1/4 in (6,35 mm) | Vlastní T-matice a vkládací matice tohoto systému |
Drážka, která je o 1 mm užší, neselže u pracovního stolu; selže ve spoji. T-matice sedí v drážce vysoko, šroub se opře o dno dříve, než matice upne, a spoj drží, dokud jej vibrace neuvolní. Na profilu nevypadá nic špatně.
Kontrola zabere minutu. Změřte ústí drážky posuvným měřítkem a čtěte uvedenou specifikaci drážky příslušenství, nikoli jeho označení “řada 20” — dva průřezy mohou být oba 20 mm čtverečních, oba prodávané jako řada 20 a přijímat rozdílný hardware.
Tloušťka stěny a hmotnost na metr
Tloušťka stěny se pohybuje zhruba od 1,3 mm u lehkých průřezů do 2,0–2,5 mm u těžkých, to vše v rámci stejného obalu 20 mm. Tento rozptyl je důvod, proč jeden průřez 20 mm může vážit o čtvrtinu více než jiný se stejným názvem na faktuře, a proč na něj nelze použít jediný údaj.
| Specifikace | Průřez A | Průřez B |
|---|---|---|
| Průřez | 20 × 20 mm | 20 × 20 mm |
| Otvor drážky | 6 mm | 6 mm |
| Hmotnost na metr | 0,44 kg/m | 0,55 kg/m |
| Druhý moment plochy, Ix = Iy | 0,68 cm⁴ | 0,72 cm⁴ |
Poznámka k tabulce: oba průřezy jsou 20 × 20 mm s drážkou 6 mm a každý sloupec uvádí údaj, který publikuje vlastní dodavatel daného průřezu — komerční údaje o průřezu, nikoli hodnoty stanovené normou, takže se na ně nevztahuje žádné normové minimum ani maximum.
Buy a heavy wall for durability, not for stiffness. The heavier section above carries about 25% more mass for about 6% more second moment of area, because at this size the 20 mm depth sets the bending stiffness and the wall does not. The extra aluminium buys slot-lip durability and fastener bearing — a nut that will not crush the groove under torque — not a beam that deflects less.
T-Slot vs V-Slot
What Each Groove Accepts
A T-slot is a channel with a narrow mouth and a wider cavity: a nut slides along the cavity and clamps wherever it is stopped. It holds brackets, panels, hinges and guards without drilling.
A V-slot replaces that channel with a V-shaped groove on the face, and a wheel with a matching profile runs inside it. The profile becomes the rail, so one bar carries the load and guides the motion.
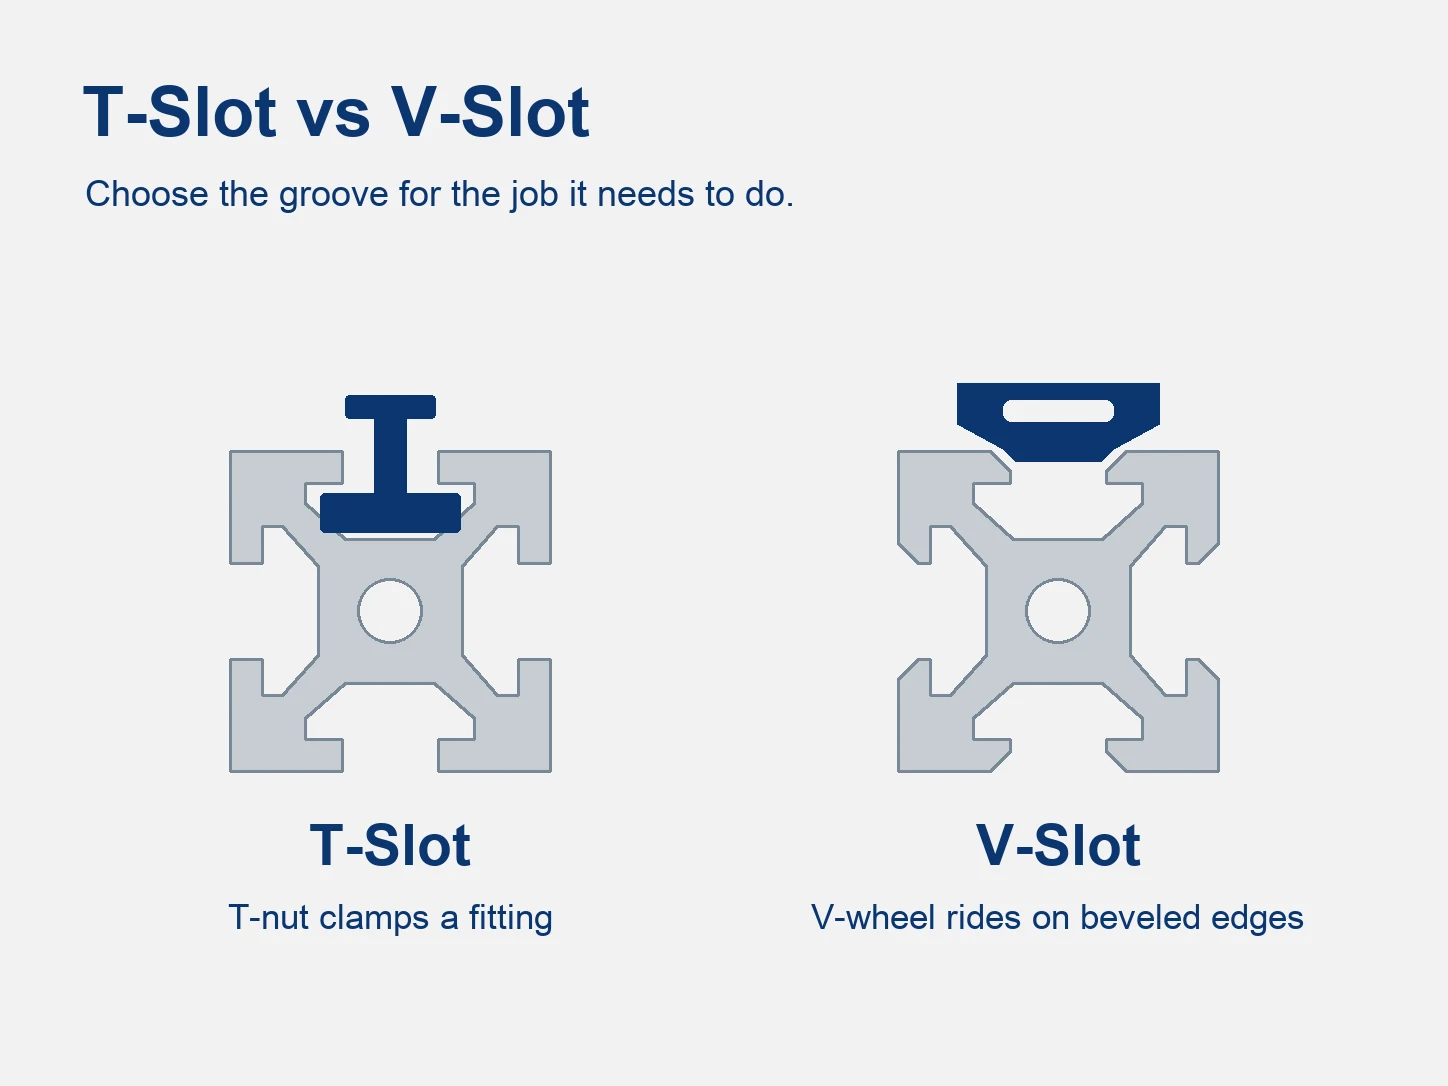
The two do not interchange. A T-nut has nothing to seat against in a V, and a wheel has no bearing surface in a T.
Where the Choice Is Already Made
The groove follows the motion, not the frame. An axis that runs on wheels needs V-slot on the faces it runs along; a guard, an enclosure or a fixture needs T-slot on every face it may grow into.
Mixed builds are ordinary — V-slot for the moving axis, T-slot for the static frame — and the detail that catches people is the corner. The outer shape of a V-slot profile differs from a T-slot profile, so a bracket designed for one does not always seat flat on the other.
Changing the groove once the frame is cut means replacing the extrusions. The brackets are the cheap part.
Section Properties and the Span They Allow
Second Moment of Area and Section Modulus
Two numbers describe how a section behaves in bending. The second moment of area, written I and measured in cm⁴, describes how the material is distributed about the bending axis, and it sets deflection. The section modulus, Z, is I divided by the distance from that axis to the outer fibre — for a 20 mm section, I divided by 1 cm — and it sets the stress at the surface.
Neither follows from mass or outer dimension. Two 20 mm squares with different wall design land at 0.68 and 0.72 cm⁴, which is why a catalogue listing only size and weight leaves the structural question open. Ask for I when a CAD library does not carry the section; it is the number the calculation needs.
The Deflection Check
Deflection, not yield, is what limits a 20 × 20 mm member. At the loads these frames carry the aluminium is nowhere near its strength limit, while the member is already bowing visibly.
For a simply supported member with a central point load:
δ = PL³ / 48EI
P is the load in newtons, L the span in metres, E the elastic modulus (about 69 GPa for 6063), and I the second moment of area in m⁴. For a 10 kg load on a 700 mm span with I = 0.68 cm⁴, the result is about 1.5 mm.
A working limit for machine framing is span divided by 500 — 1.4 mm over 700 mm, 2 mm over a metre.
| Span | Deflection at 10 kg mid-span | L/500 allowance |
|---|---|---|
| 300 mm | 0.12 mm | 0.60 mm |
| 500 mm | 0.55 mm | 1.00 mm |
| 700 mm | 1.51 mm | 1.40 mm |
| 1000 mm | 4.42 mm | 2.00 mm |
Table note: simply supported, central point load of 10 kg (98 N), 6063 with E = 69 GPa and I = 0.68 cm⁴. A uniformly distributed load of the same total gives about 63% of these figures. The values are calculated for one published section, not measured test data.
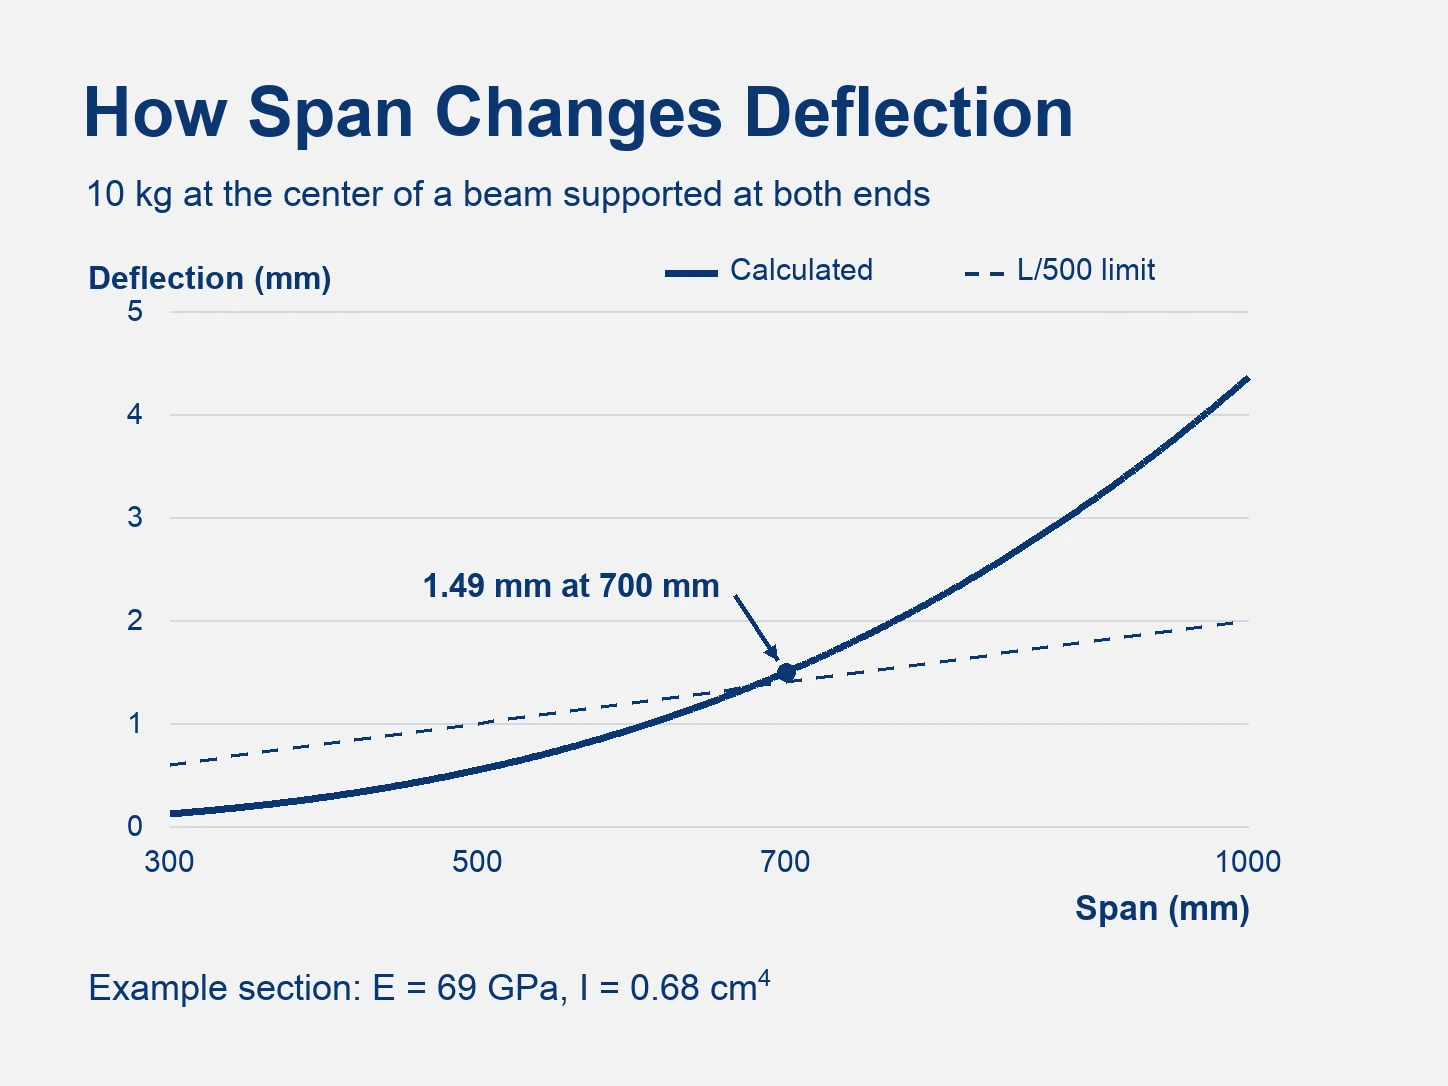
At 10 kg mid-span this section holds an L/500 allowance to roughly 700 mm. Past that span the section is the problem rather than the joint, so the answer is a deeper profile or a second support, not more brackets.
Slitina a stav
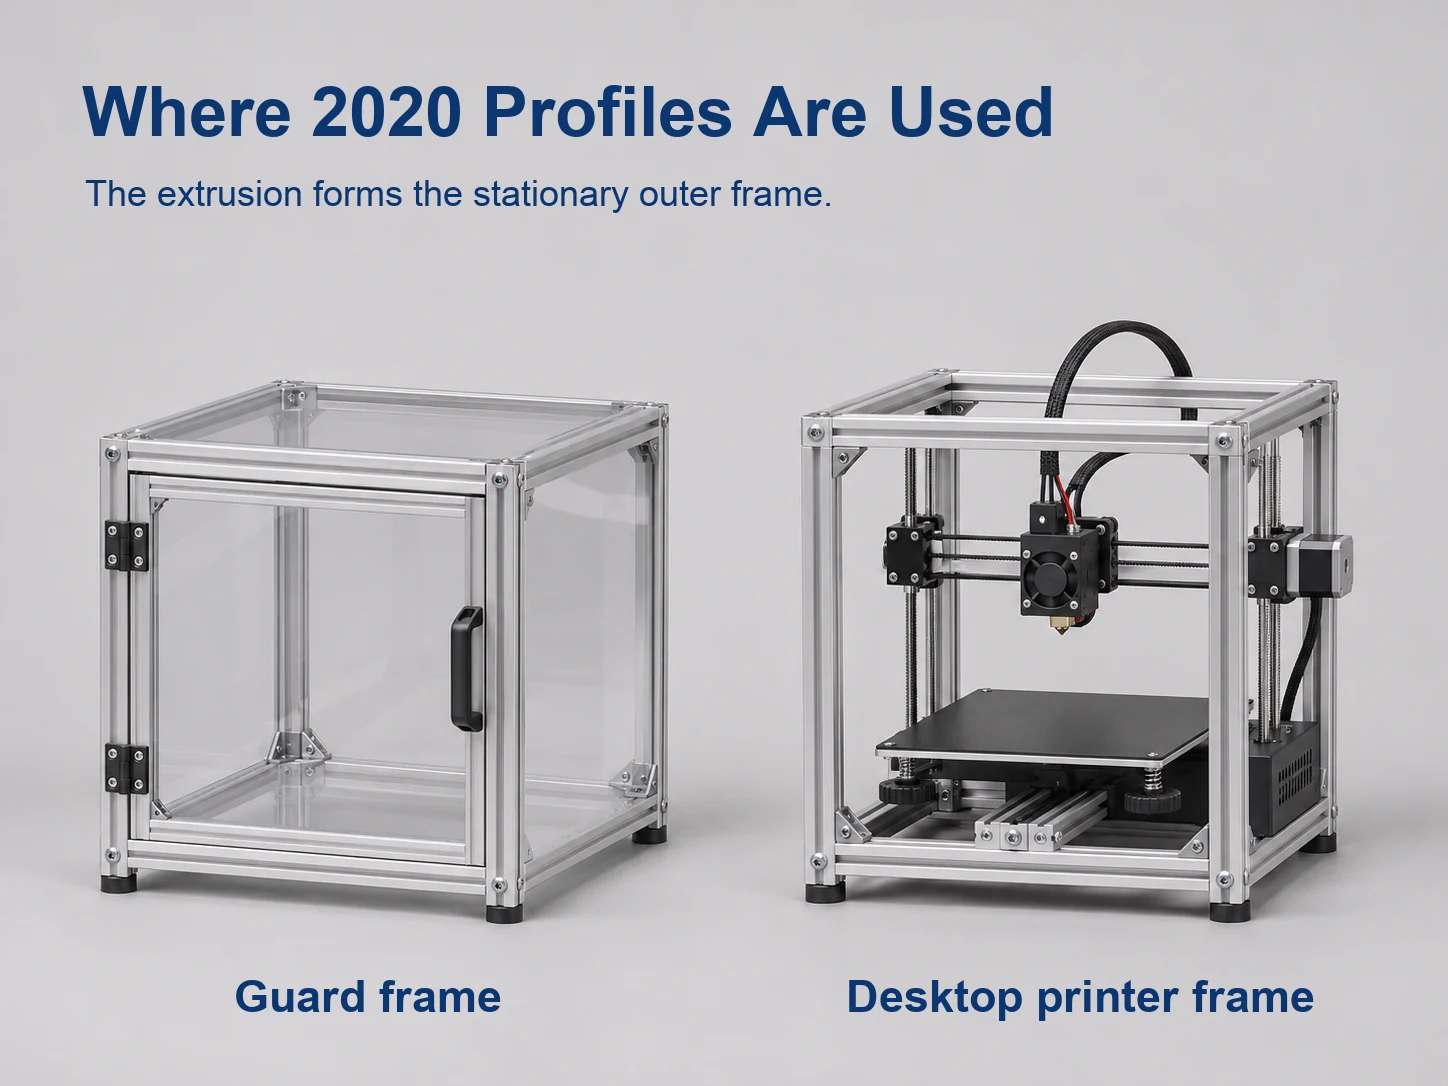
20-series profile is normally pressed from 6063-T5, and at this size that is the right default. It fills a thin four-slot section at press speed, anodizes to an even colour, and covers the work this section actually does: 3D printer frames, machine guards, enclosures, light fixtures and test jigs held together by T-nuts rather than by welds.
When 6061-T6 Is Worth the Extra Cost
6061-T6 is the stronger of the two and machines better, so it earns its price when the member carries load into a joint, or when tapped holes will be loaded and unloaded repeatedly. It is not a drop-in substitute: its higher alloying content makes it harder to press into a thin four-slot wall, and it anodizes greyer and less evenly than 6063, which shows on a visible frame.
The sequence is to specify 6063-T5 unless the joint or the thread demands more, and to confirm that the section exists in 6061-T6 before the drawing is released. A 20 × 20 mm four-slot profile is not a stock item everywhere in that alloy.
If the drawing line reads only “2020 profile”, the alloy, the temper and the standard the order is inspected against are all left open. Name the three. ASTM B221 and EN 755-2 do not set the same acceptance floor for the same temper, and a floor is what a mill certificate has to meet — not what an average bar measures.
Go/No-Go: Where 2020 Fits
A build fits this section if:
- Every loaded member spans about 700 mm or less at the load it carries.
- The load path runs through a frame of several members rather than one beam.
- The joints use 20-series hardware already specified for that slot.
- The frame stands still in service, and the load on it comes from what it holds rather than from a cutting or moving process.
A build does not fit if:
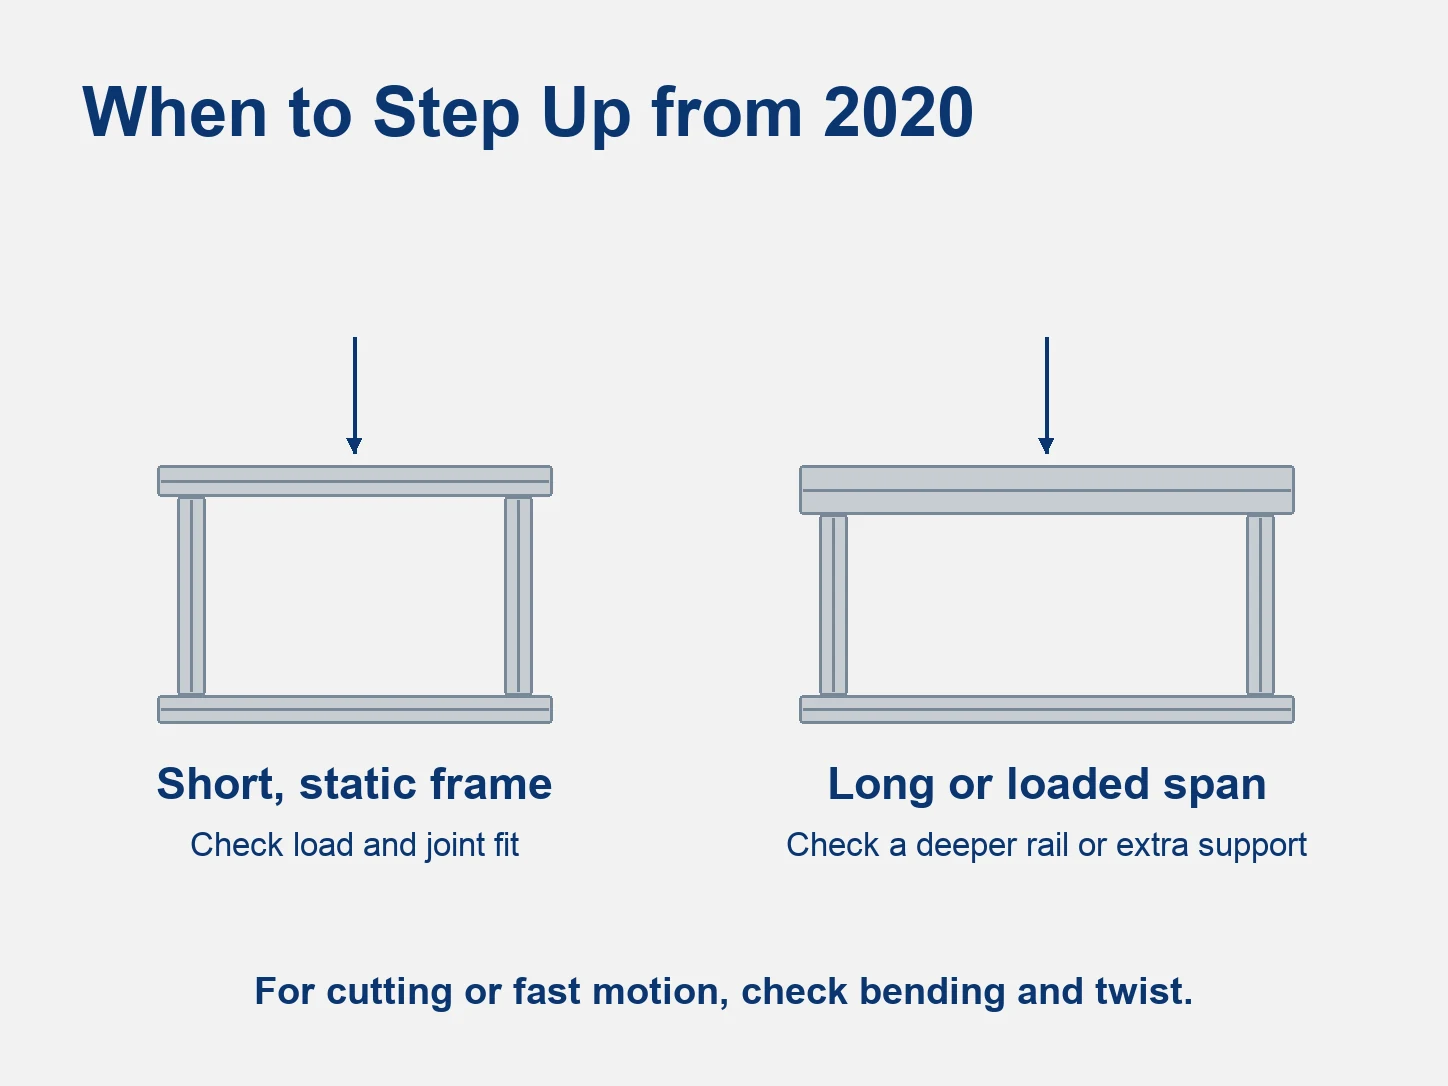
- One unsupported span carries the working load.
- The member carries a cutting load, as on a machine that mills aluminium.
- Torsional stiffness drives the design, as on a long gantry that must not twist.
- The frame has to stay square under a carriage moving at speed.
When to Step Up to 2040 or 4040
Doubling the face in the bending direction moves material further from the bending axis and does more for stiffness than anything available inside the 20 mm envelope. One axis under load goes to 2040; both axes, or a machine base, go to 4040.
Na stránkách 4040 aluminium extrusion guide carries the section properties and slot options of the next size up.
Finish and What It Changes
Anodizing Classes
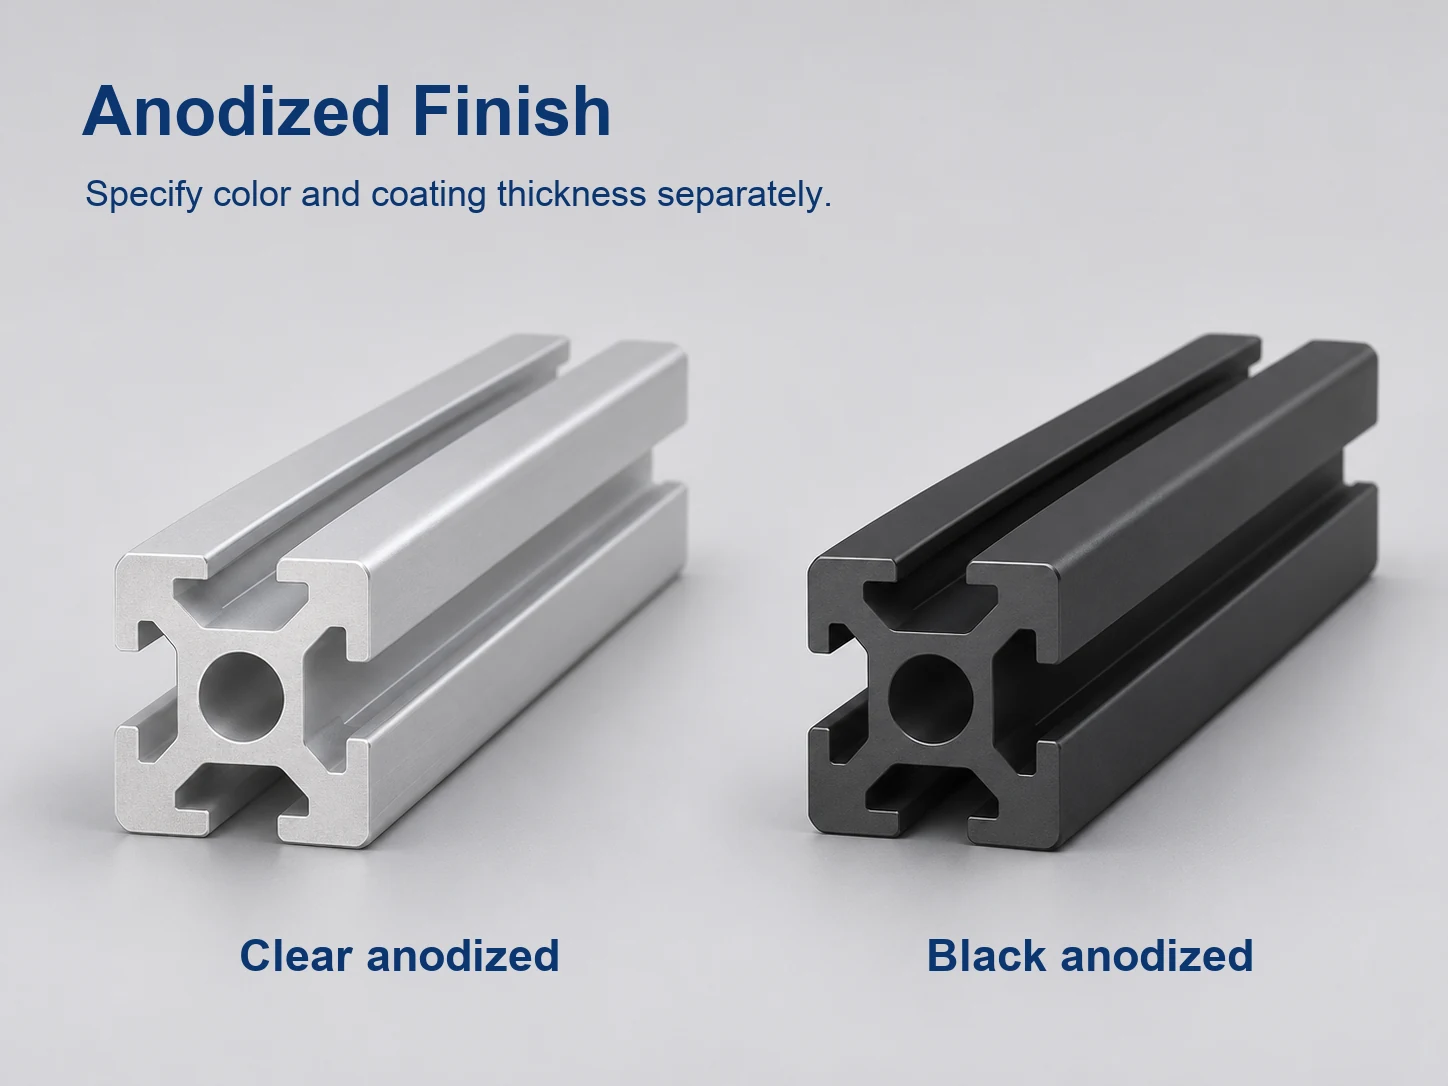
Anodizing is specified by class, and the class is a thickness. ISO 7599 grades the coating AA5 to AA25, where the number is the minimum average film thickness in micrometres — AA10 is 10 µm average — and the minimum local reading may not fall below 80% of that average.
The class follows the service condition: AA10 for indoor framing, AA15 to AA20 for sheltered and general outdoor work, AA25 for coastal exposure and heavy handling. Black is a dye inside the same class rather than a class of its own, and dark dyes generally need AA20 or higher to hold their colour.
Coating Build-Up and Slot Fit
The anodic film grows out of the aluminium rather than sitting on it, and roughly half of it forms above the original surface. At a decorative class that is a few micrometres per face, which changes nothing about a 6 mm slot — an ordinary 20-series joint has more clearance than that.
It starts to matter at hard anodizing, where the film is several times thicker, and on any joint designed as a sliding fit rather than a clamped one. Where a slot has to stay bare — for electrical contact, for earthing, or for a moving fit — say so on the order, because the whole bar is anodized unless the slot is masked.
We run anodizing and powder coating in-house, so class and masking sit on the same order as the cut list.
What to Put on the Drawing or PO
An order that comes back as the part you designed names all of these:
- Section and slot width — 20 × 20 mm, with the slot measured or specified (6 mm, 5 mm or 1/4 in).
- Alloy, temper and standard — 6063-T5 to ASTM B221, to EN 755-2, or the equivalent grade agreed.
- Délka řezu a její tolerance — one nominal length per line, with the band.
- Cut-end condition — deburred, or chamfered where the end sits against a bracket face.
- End machining — tapping, counterboring or mitring, if the design calls for it.
- Dokončení — anodizing class and colour, with masked areas named.
- Documentation — MTC on every order, and a third-party report where the project requires one.
- Marking and packing — bundle labels that match the cut list, so two similar lengths are not swapped at assembly.
Cut length deserves its own line because it is the tolerance most often left out. A saw cut is not a milled end: its band is wider than the cross-section tolerance, and it is set at the saw rather than at the die. Left unstated, the length is whatever the supplier’s standard practice produces — and a frame that has to close to 0.5 mm across a diagonal will not close.
Once the section and the cut list are settled, the 2020 aluminum extrusion product page lists the alloy, the finish options and the cut-to-length service.
Závěr
The 20 × 20 mm name covers a 25% spread in mass and three slot families, so what arrives is decided by the order rather than by the designation — and none of it is visible until the bars are cut and anodized.
We supply 20-series profile cut to length against the tolerance on the order, anodize it in-house including black, and issue an MTC with every shipment stating the alloy and temper supplied.
Send us the cut list with the slot width and the span each member carries, and we will come back with the section, cut tolerance and anodizing class.
ČASTO KLADENÉ DOTAZY
Can I mix 2020 profile from two suppliers in one frame?
Only if both use the same slot family and the same anodizing class. Slot geometry and film thickness both vary between systems, and two batches in one frame will not match in shade. Confirm both before ordering half a frame from each.
What slot width does a 2020 profile have?
Usually 6 mm on the metric 20-series, which takes M5 T-nuts. Some ranges use a 5 mm slot, and the North American 20-series uses 1/4 in (6.35 mm). Measure the slot mouth before ordering hardware.
Do you supply 2020 profile cut to length?
Yes. Send three things:
- Cut lengths, with the tolerance you need
- Šířka drážky
- Slitina a temper
We cut to length, deburr and anodize before packing, and issue an MTC with every order.
Is 2020 strong enough for a 3D printer frame?
Yes, for desktop FDM and CoreXY sizes, where members span well under 700 mm. Large-format or high-speed machines usually need 2040 on the gantry axis to hold deflection.