


7055 is one of the highest-strength wrought aluminium alloys in commercial supply, built on a higher zinc-and-copper load than the 7xxx grades around it. Alcoa introduced it in 1991 — T7751 for plate, T77511 for extrusions — aimed squarely at compression-dominated structure: upper wing skins, horizontal stabilizers, and keel beams.
The decision it forces is narrow. 7055 buys guaranteed strength in thick section that no standard 7075 or 6061 product reaches, and in exchange it comes in a short list of forms and aerospace specifications, is not a fusion-welding alloy, and still needs corrosion protection designed in. If the part is welded, or priced against 7075, 7055 is not the answer.
7055 알루미늄 합금이란?
7055 is a heat-treatable Al-Zn-Mg-Cu alloy, registered by the Aluminum Association and listed in the UNS system as A97055. Zinc and magnesium form the MgZn₂ strengthening precipitate; copper raises strength and fracture toughness; zirconium forms Al₃Zr dispersoids that pin grain boundaries and resist recrystallisation through hot working.
| 요소 | 범위 (중량 기준 %) | 역할 |
| 아연(Zn) | 7.6–8.4 | 主要强化元素 |
| 마그네슘(Mg) | 1.8–2.3 | Forms the MgZn₂ strengthening phase with zinc |
| 구리(Cu) | 2.0–2.6 | Raises strength and fracture toughness; the main driver of corrosion sensitivity |
| 지르코늄(Zr) | 0.08–0.25 | Grain refinement; improves hardenability in thick plate |
| 실리콘(Si) | ≤0.10 | 杂质限量 |
| 철(Fe) | ≤0.15 | 杂质限量 |
| 티타늄(Ti) | ≤0.06 | 晶粒细化剂 |
| 크롬(Cr) | ≤0.04 | 결정립 구조 제어 |
| 망간(Mn) | ≤0.05 | 미량 한도 |
| 기타 (각각 / 전체) | ≤0.05 / ≤0.15 | 미량 한도 |
| 알루미늄(Al) | Balance (85.9–88.5) | 비귀금속 |
Limits follow the Aluminum Association registration. Density is 2.86 g/cm³ (0.103 lb/in³), against about 2.81 g/cm³ for 7075 — the alloy carries a denser zinc-and-copper load in exchange for its strength, which is why design comparisons run on specific strength rather than on absolute MPa.
Two points about form matter before anything else. 7055 is not a catalogue alloy, and its aerospace material specifications cover two families only: AMS 4206 for plate and AMS 4324, 4336, and 4337 for extruded bar, tube, and profile. Anything outside those sections and sizes is produced to your drawing. Name the form and its governing specification on the enquiry, because the temper suffix changes with the form.
Stiffness does not improve with the alloy. The elastic modulus is 71.7 GPa (10.4 × 10³ ksi), essentially the same as 6061 at 68.9 GPa, so 7055 buys strength and weight — never rigidity. A part that deflects too far in 6061 will still deflect too far in 7055.
Tempers and Aging Routes
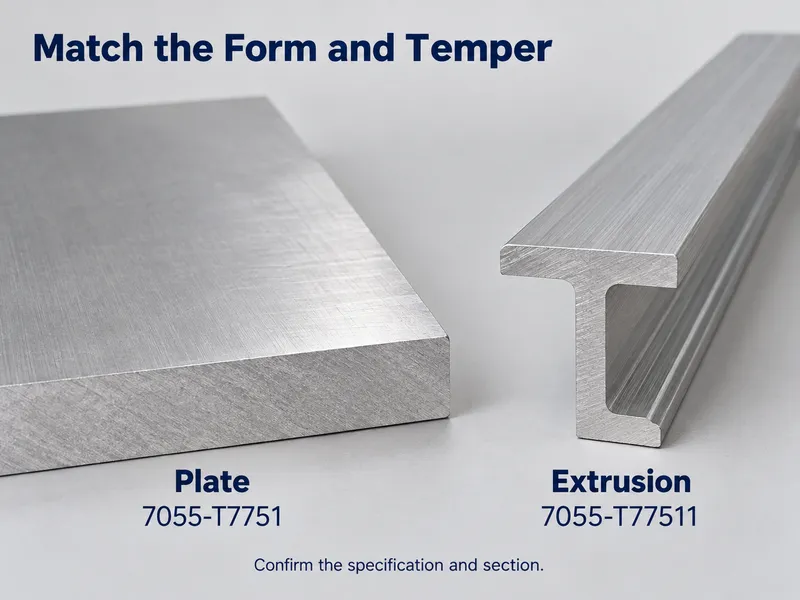
7055 is never supplied peak-aged in its aerospace specifications. Every published temper is a T7-type treatment, and the difference between them is how much overaging the alloy is given to buy corrosion margin.
- T74 type — two-step overaging. Most resistant to stress-corrosion cracking, lowest strength of the three.
- T76 type — two-step overaging, less severe. Higher strength than T74, with exfoliation resistance as the design target.
- T77 type — retrogression and re-aging (RRA): the alloy is peak-aged, briefly retrograded at high temperature, then re-aged. This recovers near-peak strength while holding T76-class exfoliation resistance, and it is the treatment that made 7055 viable for wing skins.
| 성질 | 양식 | Governing specification | Aging route | Design minimum, Rm / Rp0.2 (L) |
| T7751 | 플레이트 | AMS 4206 | RRA | 614 / 593 MPa (0.5–1.5 in) |
| T77511 | 압출 | AMS 4337 | RRA | 648 / 620 MPa (0.5–1.5 in) |
| T76511 | 압출 | AMS 4336 | Two-step overage (T76) | 614 / 586 MPa (≤0.25 in) |
| T74511 | 압출 | AMS 4324 | Two-step overage (T74) | 572 / 524 MPa (≤0.25 in) |
Choose by section and environment rather than by the strength column: the RRA tempers, T7751 and T77511, are the strength choice, and T74511 is what to specify where sustained tensile stress in a wet or chloride-bearing environment is the governing risk. Read each minimum against the thickness column printed beside it — the thin-extrusion and thick-plate figures are different measurements, not a ranking of the tempers.
The single and double suffix is the form. Per ANSI H35.1, a T_51 treatment applies to rolled plate and a T_511 treatment to extruded rod, bar, tube, and shape, which is why plate is T7751 and the extrusion is T77511. A drawing that asks for “7055-T7451” without the second 1 is usually describing an extrusion; confirm which form is meant before quoting.
7055-T7751: Design Minimum Versus Typical
Minimums govern the design; typicals tell you what actually arrives. Both columns below are for the L direction in 7055-T7751 plate.
| 속성 | Design minimum, AMS 4206 (0.5–1.5 in) | Typical, Alcoa (25.4 mm) |
| Tensile, Rm | 614 MPa (L and LT) | 669 MPa (L) / 627 MPa (LT) |
| Yield, Rp0.2 | 593 MPa (L) / 586 MPa (LT) | 655 MPa (L) / 614 MPa (LT) |
| Compressive yield, Fcy | 593 MPa (L) / 614 MPa (LT) | 669 MPa (L) |
| 신장 | 7% (L) / 8% (LT) | 11% (L) / 10% (LT) |
Design to the minimum column and treat the typicals as a planning guide: the guarantee that governs your lot is the one printed on the mill test certificate, not the number on a producer datasheet. Note where the compressive value sits — in the LT direction the minimum compressive yield runs 28 MPa above the minimum tensile yield, which is the property that compression-critical wing and beam sizing is built on.
7055 vs 7075 vs 6061
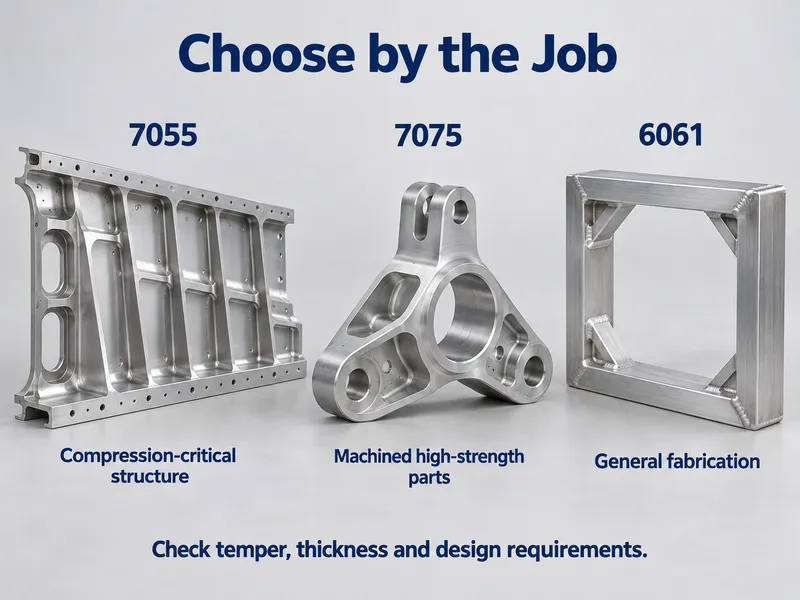
| 합금 / 조질 | Typical yield Rp0.2 (MPa) | Typical tensile Rm (MPa) | 용접성 | Bare corrosion | Where it fits |
| 6061-T6 | ~276 | ~310 | 우수 | Good | General structural and welded work, stocked widely |
| 7075-T6 | ~503 | ~572 | Poor | 제한적 | Airframe parts with complex geometry; the widest 7xxx supplier choice |
| 7055-T7751 | ~655 | ~669 | Poor | Limited, but ahead of T6-type | Compression-critical thick plate and extrusion |
Typicals are at roughly 25 mm in the L direction. Against that basis, 7055-T7751’s design minimum of 593 MPa already sits above 7075-T6’s typical yield of about 503 MPa at a similar thickness, so the strength question is settled rather than close. The trade moves to everything else: 7055 arrives in far fewer forms and tempers, costs more, and is bought to an aerospace specification rather than pulled off a shelf. Published reviews of aircraft alloy development put the 7055-T77 gain at roughly 8–12% over 7150-T77, the grade it was developed to improve on.
If the section is thin, the shape is complex, or the schedule is short, 7075-T6 is the practical answer. If the governing load is compression in thick plate, 7055 is the reason that class of part exists.
Where 7055 Is Used
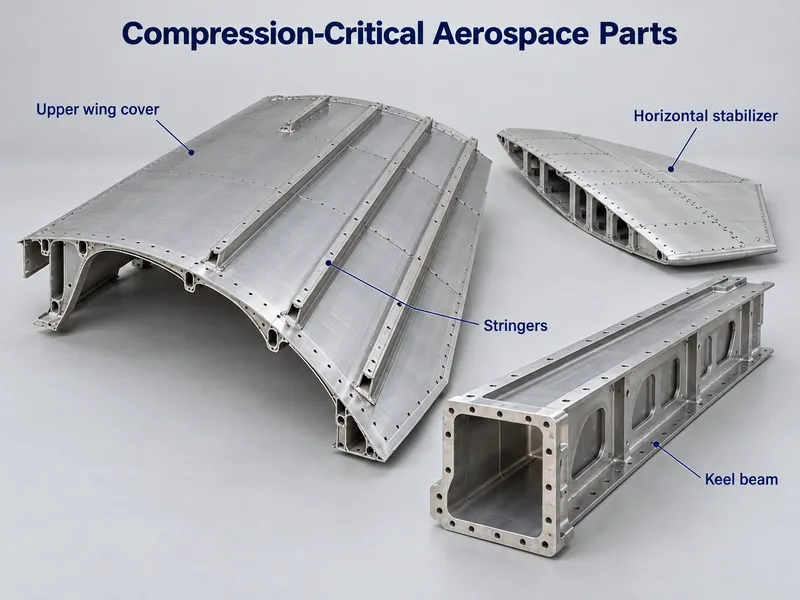
7055 was developed for the Boeing 777 upper wing, where it is still used as T7751 plate and T77511 extrusion. Upper wing skins, the horizontal stabilizer, and keel beams are the same family of part.
Look past the aircraft name and each one is the same member — thick, machined from plate or cut from a heavy extrusion, loaded mainly in compression or bending, and fastened rather than welded.
That part-type reading is the durable one, because programmes date quickly: newer widebody wings have moved largely to composite. The question worth asking is whether your part is a thick, compression-loaded metal member. If it is, 7055 belongs in the comparison; if it is not, the premium buys nothing.
Working With 7055
Welding and Joining
7055 is not a fusion-welding alloy. Arc welding destroys the precipitate structure in the weld and the heat-affected zone, and the high copper content leaves those zones both weak and prone to stress-corrosion cracking, so aerospace specifications avoid fusion welds in critical 7055 components. Structure is fastened or bonded instead.
Friction stir welding produces sound 7xxx joints where post-weld aging is applied, and it is the research route for integrally stiffened panels. It is not a process a general fabrication shop can quote, so treat it as a production decision rather than a fallback. If welding is the primary joining method, the grade is wrong: 7003 그리고 7005 weld with 5xxx filler and give up strength you may not need.
Machining and Forming
7055 machines cleanly in the T7-type tempers. It is hard and produces short, well-broken chips rather than the long strings a soft grade throws, so surface finish is easy to hold — provided the setup is rigid, the tooling is sharp carbide, and coolant reaches the cut under pressure.
Distortion is the real risk. Thick plate and heavy extrusions carry residual stress from quenching and stretching, and material removed unevenly will move. Keep stock removal balanced across the section, take finishing passes light, and expect to machine a part that has to stay flat in two setups rather than one.
Forming is limited. The T7-type tempers do not carry enough ductility for tight bends, so a part with formed detail is normally machined from plate instead. Design the geometry for the machining route from the start.
Corrosion and Stress-Corrosion Limits
Bare corrosion resistance is limited. With copper at 2.0–2.6%, 7055 is in the same family as 7075 and needs anodising, primer and paint, or sealants in any moist or chloride-bearing service, plus isolation wherever it is bolted to a dissimilar metal.
What the T7-type tempers buy is real, though. MIL-HDBK-5 notes that the T77-type temper has exfoliation resistance comparable to the T76-type tempers of other 7xxx grades, so 7055-T7751 performs better in that respect than 7075-T6 — the comparison the strength table does not show.
Stress-corrosion cracking stays a design limit rather than an edge case. Keep sustained tensile stress inside the allowables for the temper and section you are buying, and state the service environment on the enquiry so the temper recommendation matches it.
사용 온도
Treat 7055 as a room-temperature structural alloy. Like every precipitation-hardened grade, it over-ages and loses strength as service temperature rises, so the ambient allowables are not the right basis for a hot part. Where service temperature is elevated, work from the elevated-temperature data for the temper and thickness you are using.
적용 가능/불가 판단 기준
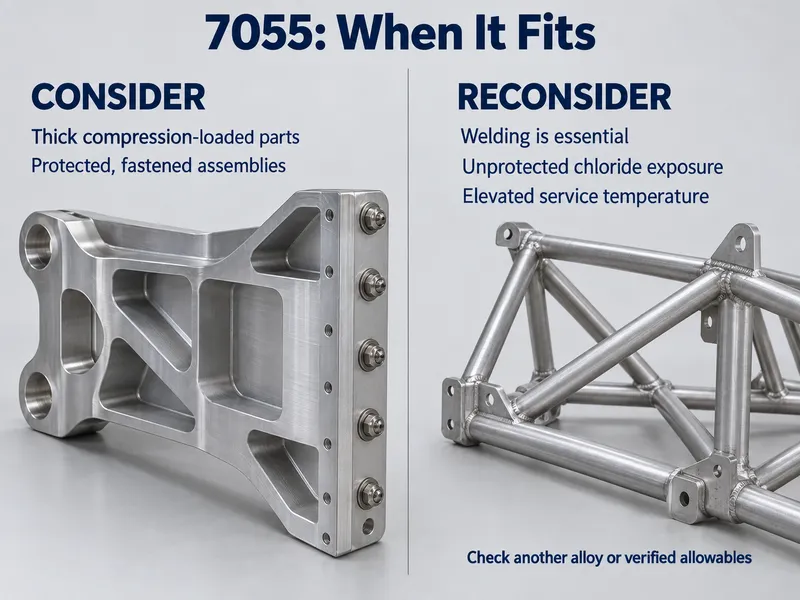
Go — specify 7055 when:
- The governing load is compression or bending in a thick section, and the part is machined from plate or cut from a heavy extrusion.
- The strength calculation is thickness-limited, so a higher compressive yield translates into real weight out of the structure.
- Joining is by fasteners or adhesive, and the assembly never sees a fusion weld.
- Corrosion exposure is designed for, with coating, sealing, and dissimilar-metal isolation built into the drawing.
No-Go — 다음의 경우 다른 소재를 찾는다:
- Welding is the primary joining method. Use 7003, 7005, or a 6000-series grade instead.
- Bare saltwater, splash-zone, or chloride service with no coating is expected. Use 5083 or a protected 6xxx grade.
- The part is thin, geometrically complex, or needed at short notice — 7075-T6 stocks in far more forms, tempers, and sizes.
- Standard strength with easy fabrication is enough. 6061-T6 costs less and processes far more easily.
- The drawing names a 7055 temper outside the AMS plate and extrusion range. Confirm the governing specification before quoting.
소싱 노트: 주문 전 확인해야 할 사항
7055 is not a catalogue material the way 7075 is, so the enquiry has to carry more information than usual. 7055 plate comes to AMS 4206 and extruded bar, tube, and profile to AMS 4324, 4336, or 4337, and the temper suffix tells you which form you are buying: T7751 is plate, T77511 is extrusion. A quote that silently converts one into the other is a quote for a different part. Form is not the constraint — sections, sizes, and profiles outside the standard range are produced to your drawing.
문의 시 네 줄이 대부분의 역할을 합니다:
- Governing specification and form — AMS 4206 for plate; AMS 4324, 4336, or 4337 for extrusion.
- 성질 — T7751 or T77511 for strength, T74511 or T76511 where SCC margin drives the choice.
- Governing thickness — published minimums are tabulated by thickness column, and thick sections carry the lower values.
- 문서 수준 — MTC as standard, plus independent test reports where the programme requires them.
On documents, the MTC that ships with every order carries the chemistry and mechanical results for that lot, which is the evidence an aerospace or defence buyer actually reviews. SGS chemical, mechanical, and ultrasonic reports are available on request at extra cost where third-party verification is required. If your project works to certificate levels, EN 10204 3.1 is signed by the manufacturer’s own inspection representative while 3.2 adds an independent countersignature.
결론
7055 알루미늄 is the strength ceiling of wrought aluminium in thick section, and the price of that ceiling is specific: a short list of forms and AMS tempers, no fusion welding on load-carrying structure, and corrosion protection that has to be designed in rather than assumed. It is a compression-driven choice, not a general-purpose upgrade.
We supply 7055 plate and extruded bar, tube, and profile to your drawing, including the T7-type tempers and non-standard sizes that fall outside the standard range, with an MTC on every order.
Send us the drawing with the temper and the load case for a grade-fit review.
자주 묻는 질문
Is 7075 a drop-in substitute for 7055?
Not where thickness or compressive load drives the design. 7055 raises minimum yield noticeably in thick plate, so a part sized on 7075-T6 may be over-built rather than safe. Re-run the strength and toughness check against your own section before switching either way.
How much does 7055 cost, and what is the minimum order?
Expect an aerospace-grade premium over 7075, so fix the temper and the form before comparing quotations. Standard sizes ship from stock; non-standard tempers and dimensions run as low-MOQ custom production, typically 10–60 days.
What documents come with a 7055 order?
A mill test certificate ships with every order, listing the chemistry and mechanical results for that lot. SGS chemical, mechanical and ultrasonic reports are available on request at extra cost, and EN 10204 3.2 adds a third-party countersignature.
Why can 7055 not be welded?
Because the copper level that gives the alloy its strength is the same element that ruins a fusion weld. The heat-affected zone over-ages, loses strength and gains stress-corrosion risk, and no post-weld treatment brings it back. Fasten or bond 7055 structure instead.






