6026-T9 to stan, który należy określić, gdy część obrabiana mechanicznie musi stawiać opór trwałemu odkształceniu w takim zakresie, na jaki pozwala ten stop, i nigdy później nie będzie zginana. Odkształcenie plastyczne na zimno pręta po starzeniu podnosi granicę plastyczności Rp0,2 do 330 MPa, o 30 MPa powyżej T6, i pozostawia wydłużenie A do dyspozycji na poziomie 4% zamiast 8%.
Wytrzymałość to tylko połowa decyzji. Sekwencja produkcyjna ustala również, w jakiej formie każdy stan jest dostępny, a stan na formie, której nie możemy wytwarzać, nie jest specyfikacją, którą można zamówić.
Czym jest 6026
6026 to stop Al–Mg–Si z serii 6xxx, który zyskuje wytrzymałość dzięki wydzielaniu Mg₂Si podczas sztucznego starzenia. Jego cechą definiującą jest dodatek ułatwiający obróbkę skrawaniem: bizmut w ilości 0,50–1,50% łamie wiór, podczas gdy ołów jest ograniczony do maks. 0,40%, a nie stanowi mechanizmu. Zachowuje to odporność korozyjną i reakcję na anodowanie zwykłego stopu 6xxx, dodając jednocześnie kontrolę wióra typową dla gatunku łatwo skrawalnego — rolę, którą pełniły 6262 i 6012, z bizmutem odpowiadającym za łamanie wióra.
Kompromis polega na tym, gdzie situuje się stop, a nie na tym, co potrafi. Bizmut nie podnosi wytrzymałości, więc 6026 jest przede wszystkim gatunkiem do obróbki skrawaniem, a dopiero w drugiej kolejności gatunkiem konstrukcyjnym; tam, gdzie decyduje maksymalna wytrzymałość, 6082 lub 7075 radzą sobie lepiej. O tym, co decyduje o części z 6026 w praktyce, decyduje stan, ponieważ rozrzut między T6, T8, T9 i T6510/T6511 wynosi od 300 do 330 MPa w granicy plastyczności i od 8% do 4% w wydłużeniu — wystarczająco szeroko, by zdecydować, czy część w ogóle można formować.
Skład chemiczny (EN 573-3)
Bizmut jest dodatkiem zamierzonym; cyna i ołów znajdują się na pułapach zanieczyszczeń. To rozróżnienie ma znaczenie przy czytaniu atestu hutniczego, ponieważ wysoka zawartość cyny jest sygnałem zanieczyszczenia, a nie korzyścią w postaci łatwej skrawalności.
| Element | 6026 (EN 573-3, % mas.) | Co robi |
|---|---|---|
| Si | 0.60–1.40 | Tworzy Mg₂Si z Mg — źródło wytrzymałości |
| Fe | 0,70 maks. | Zanieczyszczenie; wpływa na wykończenie powierzchni i ciągliwość |
| Cu | 0.20-0.50 | Podnosi wytrzymałość i utwardza wydzielenie |
| Mn | 0.20–1.00 | Kontroluje strukturę ziarna i rekrystalizację |
| Mg | 0.60–1.20 | Równoważy się z Si w Mg₂Si |
| Cr | maks. 0,30 | Zanieczyszczenie w tym gatunku |
| Zn | maks. 0,30 | Zanieczyszczenie |
| Ti | 0,20 maks. | Rafinator ziarna |
| Bi | 0.50–1.50 | Dodatek ułatwiający obróbkę skrawaniem — łamie wiór |
| Pb | maks. 0,40 | Pozostałość; pułap dopuszczany przez wyłączenia ELV i RoHS |
| Sn | 0.05 max | Pułap zanieczyszczenia, nie dodatek |
| Inne | Maks. 0,05 każdy, maks. 0,15 łącznie | — |
| Al | Równowaga | — |
Sprawdź trzy linie na atestacie, zanim zaakceptujesz wytop: Bi w zakresie 0,50–1,50%, Sn na poziomie 0,05% lub poniżej oraz Pb na poziomie 0,40% lub poniżej. Wytop z Bi poniżej 0,50% obrabia się długim i ciągliwym wiórem; wytop z Sn powyżej 0,05% sygnalizuje zanieczyszczenie złomem, a nie zmianę konstrukcyjną.
Jak produkowane są stany T
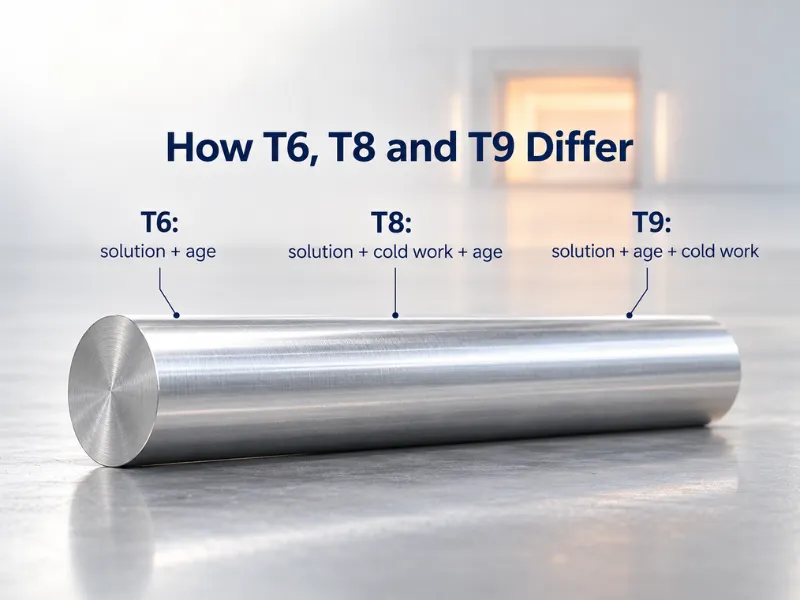
Każdy stan utwardzany wydzieleniowo z serii 6xxx zaczyna się tak samo: wlewek jest poddawany obróbce cieplnej roztworowej w celu rozpuszczenia pierwiastków stopowych, hartowany w celu uwięzienia ich w przesyconym roztworze, a następnie starzony, aby wydzieliły się jako drobne cząstki. Przyrostek po T rejestruje, co dzieje się wokół tej sekwencji podstawowej — a kolejność odkształcenia plastycznego na zimno względem starzenia jest tym, co odróżnia T8 od T9.
- T6 — obróbka cieplna roztworowa, następnie sztuczne starzenie. Bez odkształcenia plastycznego na zimno.
- T8 — obróbka cieplna roztworowa, odkształcenie plastyczne na zimno, następnie sztuczne starzenie. Odkształcenie plastyczne na zimno następuje przed starzeniem.
- T9 — obróbka cieplna roztworowa, sztuczne starzenie, następnie odkształcenie plastyczne na zimno. Odkształcenie plastyczne na zimno jest operacją końcową.
- T6510 — T6, a następnie usunięcie naprężeń przez rozciąganie, trwałe odkształcenie 1–3% na prętach okrągłych, prętach, profilach i rurach (0,5–3% na rurach ciągnionych), bez dalszego prostowania po rozciąganiu.
- T6511 — to samo co T6510, z wyjątkiem tego, że lekkie prostowanie po rozciąganiu jest dozwolone w celu spełnienia tolerancji wymiarowych.
T9 jest jedynym z pięciu, który poddaje pręt odkształceniu plastycznemu na zimno po starzeniu. Starzenie ustaliło już wydzielenie; ciągnienie na zimno dodaje następnie umocnienie od dyslokacji na jego wierzchu i ustala średnicę w tym samym przejściu. Pręt T9 przychodzi z już ustalonymi wymiarami i naprężeniami resztkowymi, dlatego precyzyjne części toczone są zwykle określane w T9 — średnica, do której obrabiasz, jest średnicą, którą pręt utrzymuje.
T8 odwraca tę kolejność. Odkształcenie plastyczne na zimno wprowadza się przed starzeniem, więc pręt jest starzony w swoim wymiarze po ciągnieniu, a nie ciągniony po starzeniu. Pręt T8 osiąga granicę plastyczności 315 MPa i wytrzymałość na rozciąganie 345 MPa przy wydłużeniu 4% — więcej granicy plastyczności niż T6, o 15 MPa mniej niż T9.
6026-T9 w liczbach
Poniższe wartości minimalne pochodzą z EN 754-2 dla prętów ciągnionych na zimno i EN 755-2 dla wyrobów wyciskanych. T9 istnieje wyłącznie jako wyrób ciągniony; T6510 i T6511 istnieją wyłącznie jako wyrób wyciskany i mają tę samą linię wytrzymałości co T6 w każdym przedziale wymiarowym.
| Temperament | Forma i norma | Zakres rozmiarów | Rm min (MPa) | Rp0,2 min (MPa) | A min (%) | HB (typ.) |
|---|---|---|---|---|---|---|
| T6 | Pręt ciągniony, EN 754-2 | D ≤ 80 mm | 370 | 300 | 8 | 95 |
| T8 | Pręt ciągniony, EN 754-2 | D ≤ 80 mm | 345 | 315 | 4 | 95 |
| T9 | Pręt ciągniony, EN 754-2 | D ≤ 80 mm | 360 | 330 | 4 | 95 |
| T6 / T6510 / T6511 | Wyciskany, EN 755-2 | D ≤ 140 mm | 370 | 300 | 8 | 95 |
| T6 / T6510 / T6511 | Wyciskany, EN 755-2 | 140 < D ≤ 200 mm | 340 | 250 | 8 | 90 |
| T6 / T6510 / T6511 | Wyciskany, EN 755-2 | 200 < D ≤ 250 mm | 300 | 200 | 8 | 90 |
Wybieraj na podstawie kolumny granicy plastyczności, a nie kolumny wytrzymałości na rozciąganie. T9 utrzymuje najwyższą granicę plastyczności na poziomie 330 MPa, o 30 MPa powyżej T6, podczas gdy jego minimum wytrzymałości na rozciąganie wynoszące 360 MPa faktycznie leży 10 MPa poniżej T6 wynoszącego 370 — odkształcenie plastyczne na zimno na starzonej strukturze kupuje odporność na trwałe odkształcenie i oddaje wytrzymałość na rozciąganie oraz wydłużenie, aby to uzyskać.
Właściwości fizyczne są takie, jak zwykle w przypadku 6xxx; są to wartości typowe, a nie minimalne: gęstość 2,72 g/cm³, moduł sprężystości około 69–70 GPa, przewodność cieplna 172 W/(m·K), przewodność elektryczna około 26 MS/m (mniej więcej 44% IACS) oraz współczynnik rozszerzalności cieplnej 23,4 × 10⁻⁶/K między 20 a 100 °C. Krzepnięcie przebiega w przybliżeniu w zakresie 575–650 °C.
T9 vs T6 vs T8 vs T6510/T6511
| Temperament | Sekwencja | Rm min | Rp0.2 min | A min | Kiedy go wybrać |
|---|---|---|---|---|---|
| T6 | Przesycanie + starzenie | 370 | 300 | 8% | You need the best tensile-elongation balance, or the part is extruded rather than drawn |
| T8 | Solution + cold work + age | 345 | 315 | 4% | The bar is already cold drawn and the part needs more proof stress than T6 at the same 4% elongation |
| T9 | Solution + age + cold work | 360 | 330 | 4% | The finished part is cut, not formed, and must hold its set under the highest load the grade allows |
| T6510 | T6 + stretch, no re-straightening | 370 | 300 | 8% | A large extruded section is machined flat or square and residual stress would move it |
| T6511 | T6510 + light straightening | 370 | 300 | 8% | Same as T6510, but the section needs straightening inside standard tolerance after the stretch |
T9 is the right call when the part is produced entirely by machining and the design load is carried below the yield point. The 330 MPa proof stress is the highest the alloy offers, and the cold-finished diameter means the bar is already where the tolerance wants it. The cost is 4% elongation: T9 leaves almost no room for a bend, a swage, or a crimp after delivery.
T6 covers the widest range of work. Its 370 MPa tensile and 8% elongation give room to form or straighten after heat treatment, and it is the temper extruded tube and profile come in. If the part needs any deformation after aging, T6 or one of its stress-relieved versions is the one that can still take it.
T8 sits between them and is easy to overlook. It is a drawn-bar temper like T9, but with cold work ahead of aging: 315 MPa proof stress and 345 MPa tensile, still at 4% elongation. Specify T8 when the drawing calls for more proof stress than T6 and the part will not be formed — but T9 is available, it gives 15 MPa more proof stress at the same elongation, so T8 usually loses that comparison on a like-for-like drawing.
T6510 and T6511 are the stress-relieved versions of T6 and exist only for extruded product. They change residual stress, not the strength line, so the choice between them and T6 is about distortion after machining rather than load capacity. T6510 forbids straightening after the stretch; T6511 allows light straightening to hold tolerance, which is why it appears more often on standard extruded sections.
Shapes and Sizes
The temper usually decides the form. T9 and T8 are drawn-bar tempers; T6510 and T6511 are extruded; T6 exists in both. Where a drawing needs a temper the standard form does not carry, the route changes — the order does not get refused.
- Bar and rod — round 6–400 mm, hex and square 6–200 mm, length 1000–6000 mm. T9 is normally a cold-drawn round bar.
- Sheet and plate — 0.5–120 mm thick, 1000–2600 mm wide, length 1000–6000 mm.
- Rura — outer diameter 10–300 mm, wall 0.5–30 mm.
- Krąg — supplied on enquiry. Tell us the required temper, width and coil weight and we confirm what the mill can run; coil is not a standing stock form for this grade.
- Custom profiles — extruded to your section drawing (how custom extrusion profiles are produced covers the route from drawing to die).
Non-standard sections and sizes are produced to order. Low-MOQ custom runs typically take 10–60 days depending on size and processing; what a size outside the standard range changes is the production route and the lead time, not whether we will quote it.
Go / No-Go
- Go when the part is turned or milled in volume, the enquiry has to clear RoHS or ELV, and 6061-T6 is short on strength while a 2xxx or 7xxx grade would be more than the design needs. The bismuth chip control is what pays for the alloy, and it pays most on automatic lathes running long batches.
- Go when the part needs an anodized finish and free-machining behavior at the same time; a leaded free-machining grade dulls that finish and carries its own compliance burden. Note the qualification: 6026 meets ELV and RoHS under the lead exemption for aluminum alloys, which permits up to 0.40% Pb. It is a low-lead grade, not a zero-lead grade, and the distinction matters if your compliance file treats exemptions differently from substance bans.
- No-go when the drawing fixes T9 or T8 on a part that still has to be formed. That is a temper mismatch rather than an alloy limitation — 6026 forms in O and T4, and the drawing changes temper, not grade.
- No-go when the service environment needs the seawater performance of a 5xxx alloy, or when 6061 or 6063 already meets the drawing. 6026 costs more than either, and the premium only returns where the free-machining behavior and the compliance position are both being used.
Specifying and Sourcing 6026
Four lines on the enquiry prevent most wrong deliveries:
- Name the standard, not only the alloy.
6026-T9 to EN 754-2fixes the product form, the size band and the property table;6026-T9on its own leaves all three open. - Pair the temper with a form the standard carries. T9 and T8 belong to drawn bar under EN 754-2; T6, T6510 and T6511 belong to extruded product under EN 755-2. Asking for
T9 extruded profilesends the enquiry back for clarification. - Give the size band, not just the nominal. The EN 755-2 minimums step down at 140 mm and again at 200 mm, so a 210 mm bar is specified against 300 MPa tensile, not 370.
- Wymagaj EN 10204 3.1. That certificate carries the heat’s actual chemistry and mechanical results, signed at the producing mill, and it is the only document that lets you check Bi, Sn and Pb against the limits above.
Nasz Stop aluminium 6026 page lists the forms and tempers we run, so the size and temper can be checked before you write the enquiry.
Wnioski
T9 gives 6026 its highest proof stress at 330 MPa and its lowest elongation at 4%, so it suits a part that is machined to final form and loaded below yield, and rules out anything that still has to bend. T6, T8 and T6510/T6511 trade that yield back for formability or for lower residual stress in large sections.
We draw and supply 6026 in T6, T8, T9, T6510 and T6511 across bar, sheet, tube and custom profiles, with MTC on every order and coil quoted on enquiry.
Send your drawing with the standard, temper and size band, and we will confirm the production route and lead time before you commit.
Często zadawane pytania
What is 6026 T9 aluminum?
6026 is a low-lead free-machining 6xxx alloy, and T9 is the temper produced by aging the bar and then cold working it. Because the cold draw is the last step, the bar arrives strengthened and dimensionally finished — which is why T9 suits precision turned parts.
Is 6026 T9 stronger than T6?
It depends which strength you mean. T9 reaches a higher 0.2% proof stress, 330 MPa against T6’s 300, so it resists permanent set better. Its tensile minimum is 360 MPa against T6’s 370 — 10 MPa lower — and its elongation drops from 8% to 4%.
Can 6026 T9 be welded?
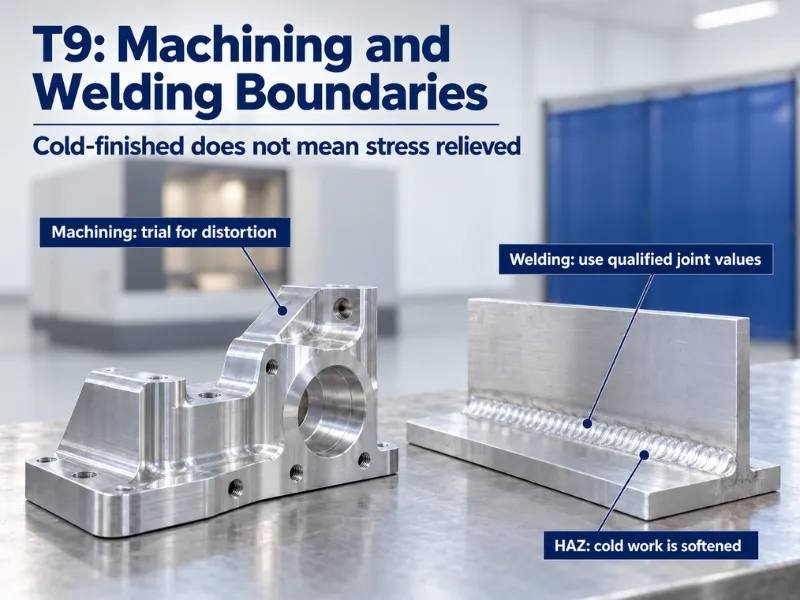
Yes, by TIG or MIG, but the joint will not hold T9 properties. The heat-affected zone reverts toward the annealed condition, and no post-weld aging treatment restores the T9 structure in this grade. If the finished assembly must carry T9 strength across a weld, change the design to a mechanical joint or pick a temper you can accept losing.
Which tempers do you supply, and what is the minimum order?
We supply bar, sheet, tube and custom profiles in T6, T8, T9, T6510 and T6511. Coil is quoted on enquiry. Round bar runs 6–400 mm and sheet 0.5–120 mm thick.
Non-standard sizes go to low-MOQ custom production, typically 10–60 days. Send the drawing, temper and size band for a route and a price.