


What 5086 Aluminum Is
5086 belongs to the aluminum–magnesium family. Magnesium is the primary alloying element and the source of both its solid-solution strength and its seawater performance; manganese and chromium are deliberate additions that control grain structure and limit intergranular attack. Copper is held to 0.10% maximum because even small amounts degrade chloride corrosion resistance.
Because it is non-heat-treatable, 5086 cannot be strengthened by solution treating and aging. Its strength comes from cold work, expressed in the H tempers, and from the magnesium held in solid solution. That single fact drives most of its engineering behavior:
- Welding does not require post-weld heat treatment — there is no precipitate to dissolve or re-form.
- Welding does soften the heat-affected zone — the cold work is annealed out locally. See the welding section, because this is the point most spec sheets get wrong.
- Temper choice is the strength choice. Ordering “5086” without a temper leaves the mill to guess.
For flat-rolled product the governing specifications are ASTM B209 (sheet and plate) and ASTM B928/B928M (high-magnesium sheet and plate for marine service, which is where the H116 and H321 tempers are defined and tested). Tube and pipe fall under ASTM B210/B221/B241, and pressure-vessel work references ASME SB-209. International equivalents are EN AW-5086 / AlMg4 / 3.3545 and UNS A95086.
Chemical Composition of 5086
Limits below follow ASTM B209. Silicon, iron, copper, zinc, and titanium are controlled impurities, not functional additions — silicon in particular does not “improve formability,” and treating it as a design variable is a common misreading of composition tables.
| Element | Weight % | Role in the alloy |
|---|---|---|
| Magnesium (Mg) | 3.5 – 4.5 | Primary strengthener; drives seawater corrosion resistance |
| Manganese (Mn) | 0.20 – 0.70 | Grain structure control, strain-hardening response |
| Chromium (Cr) | 0.05 – 0.25 | Limits intergranular corrosion and grain growth |
| Silicon (Si) | 0.40 max | Impurity — controlled, not functional |
| Iron (Fe) | 0.50 max | Impurity — excessive levels hurt ductility |
| Copper (Cu) | 0.10 max | Impurity — held low to protect corrosion resistance |
| Zinc (Zn) | 0.25 max | Impurity |
| Titanium (Ti) | 0.15 max | Grain refiner during casting |
| Others (each / total) | 0.05 / 0.15 max | — |
| Aluminum (Al) | Remainder | Base metal |
The magnesium range is the number worth remembering. At 3.5–4.5%, 5086 straddles the ~3.5% threshold above which magnesium can precipitate at grain boundaries as the beta phase (Al₃Mg₂) during sustained warm service. That is the mechanism behind the temperature limit discussed later, and it is why temper selection is not cosmetic on this alloy.
Physical Properties
| Property | Value |
|---|---|
| Density | 2.66 g/cm³ (0.096 lb/in³) |
| Melting range | 574 – 638 °C (1,065 – 1,180 °F) |
| Thermal conductivity | 117 – 127 W/m·K at 25 °C (temper dependent) |
| Electrical conductivity | 29 – 31% IACS at 20 °C |
| Coefficient of thermal expansion | 23.8 × 10⁻⁶ /°C (20–100 °C) |
| Specific heat capacity | ~900 J/kg·K |
| Modulus of elasticity (tension) | 71 GPa (10,300 ksi) |
| Poisson’s ratio | 0.33 |
Two of these numbers decide more than the rest. The thermal conductivity sits noticeably below 5052’s ~138 W/m·K, which matters for welded heat sinks and any part expected to move heat. And the 23.8 × 10⁻⁶ /°C expansion coefficient is high enough that long aluminum runs in a mixed-material assembly need expansion allowance — a detail that shows up as buckled deck panels when it is ignored.
Mechanical Properties by Temper
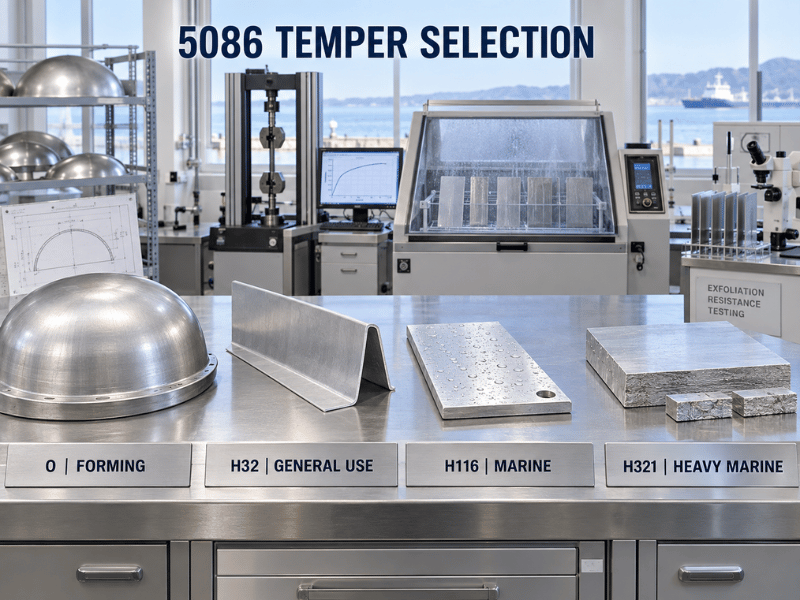
Values below are typical ranges for sheet and plate; guaranteed minimums vary with thickness and specification, and the numbers that govern acceptance are the ones on the mill test certificate. Note that H32 and H116 are close in strength — the difference between them is corrosion testing, not mechanical performance.
| Temper | Tensile strength (MPa) | Yield strength (MPa) | Elongation (%) | Typical use |
|---|---|---|---|---|
| O | 240 – 305 | 95 – 145 | 14 – 22 | Deep drawing, formed heads, spun tank ends |
| H111 | ~275 | ~125 | ≥ 12 | Lightly worked structural parts |
| H112 | 250 – 290 | 95 – 125 | 8 – 12 | Thick plate, machined parts, as-fabricated shapes |
| H32 | 275 – 345 | 195 – 240 | 6 – 12 | General marine panels, truck bodies, trailer panels |
| H34 | 305 – 365 | 220 – 275 | 4 – 10 | Higher-strength flat structures |
| H116 | 275 – 365 | 195 – 215 | 8 – 12 | Hull plating, decks, immersed marine structure |
| H321 | 275 – 365 | 195 – 215 | 8 – 12 | Heavy marine plate requiring exfoliation resistance |
ASTM B928 sets the acceptance floor for marine plate at 240 MPa tensile / 195 MPa yield / 10% elongation for 5086-H116 and H321 in the 3–50 mm range. Those minimums are lower than the typical values above because they must hold across the full thickness band — do not use typical values as a design minimum, and do not use B928 minimums to estimate what a thin-gauge coil will actually deliver.
What Each Temper Is Actually For
O is annealed and fully soft. It is the temper for deep drawing, tight-radius bending, and spun or formed tank ends; if the part needs significant plastic deformation, it starts here. H111 and H112 are lightly worked or as-fabricated conditions where mechanical properties are not the controlling requirement — common on thick plate that will be machined.
H32 is the general-purpose workhorse, roughly 20% stronger than 5052-H32 and the default for non-immersed marine panels, vehicle bodies, and industrial frames. H34 carries more strength with a real loss of formability.
H116 and H321 are the marine tempers, and the distinction matters more than the strength column suggests. Both are processed to control grain-boundary precipitation and must pass exfoliation and intergranular corrosion testing under ASTM B928. H116 is strain-hardened and stabilized; H321 is strain-hardened then thermally stabilized, which gives more predictable behavior in thick sections. For anything in continuous seawater contact, one of these two is the specification — H32 is not a substitute even though the strength numbers look similar.
Corrosion Resistance and the 65 °C Limit
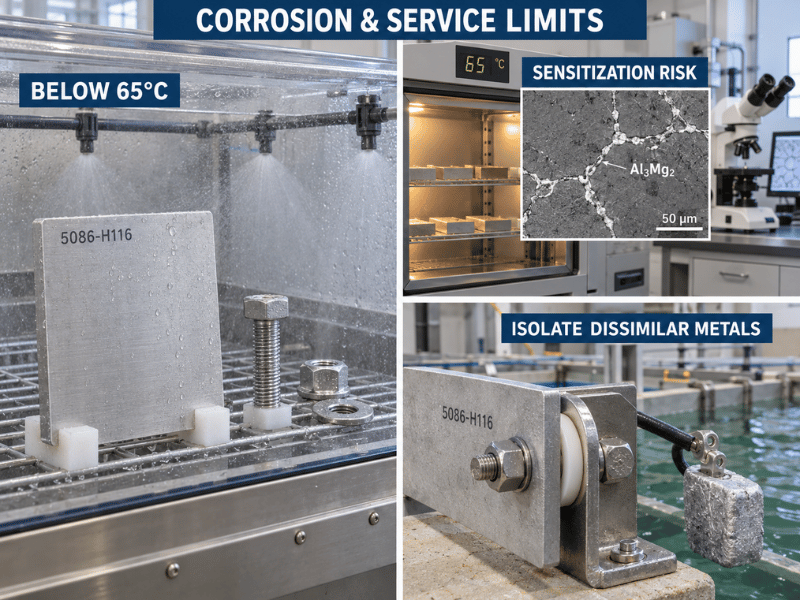
5086 forms a dense, self-healing aluminum oxide film, and the combination of high magnesium with near-zero copper gives it excellent performance in seawater, marine atmosphere, and many industrial chemicals. Unpainted 5086 hull plate has decades of service history. Long-term marine exposure testing shows low mechanical property loss after ten years.
The limitation is thermal, and it is the one constraint that catches projects out.
Above roughly 65 °C (150 °F) in sustained service, magnesium in solid solution can precipitate along grain boundaries as the beta phase (Al₃Mg₂). That network is anodic to the surrounding matrix, so the alloy becomes susceptible to intergranular corrosion, exfoliation, and stress corrosion cracking. The process is time-and-temperature dependent and it is not reversible — a plate that has sensitized cannot be recovered by heat treatment.
Practical consequences:
- Keep 5086 away from uninsulated exhaust runs, engine-room hot spots, and process equipment that dwells above 65 °C.
- For warm service, specify H116 or H321 and state the service temperature on the inquiry so the mill can supply to the right stabilization practice.
- Where sustained temperatures above 65 °C are unavoidable, look at a lower-magnesium alloy (5052) or a heat-treatable grade (6061) rather than trying to engineer around sensitization.
Galvanic corrosion is the second caveat. 5086 is anodic to steel, stainless, and copper alloys; in a mixed-metal assembly with an electrolyte present it will sacrifice itself. Insulate the joint or install sacrificial anodes — this is a design issue, not a material defect.
Welding 5086
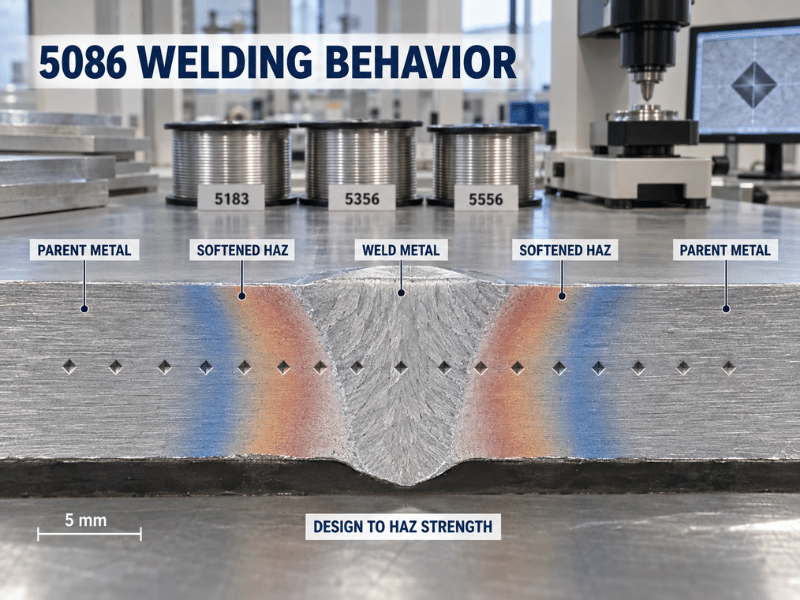
5086 welds well by GMAW (MIG) and GTAW (TIG), shows no meaningful hot-cracking tendency, needs no preheat on thin sections, and requires no post-weld heat treatment. That is genuinely excellent weldability, and it is why the alloy is dominant in welded marine structure.
What it does not do is hold its cold-worked strength through the weld. The heat-affected zone is annealed by the welding cycle — the strain hardening is removed locally and the HAZ reverts toward the O condition. In practice an H32 assembly retains roughly 70–75% of parent yield strength across the softened band, with yield dropping from ~210–230 MPa toward ~115–145 MPa.
The design rule follows directly: size welded 5086 structure on the annealed HAZ properties, not the parent-temper properties. A joint calculated on 230 MPa yield will be carrying load in a zone that yields near 130 MPa. AWS D1.2 publishes allowable stresses for this purpose and is the reference to work from.
Filler selection is the other half of the joint:
- ER5183 — the usual first choice for welding 5086 to itself. Closest strength match to the base metal and good corrosion behavior in marine service.
- ER5356 — the general-purpose 5xxx filler. Slightly lower as-welded strength than 5183, widely available, acceptable for most non-critical joints.
- ER5556 — higher as-welded strength than 5356, used where joint strength governs and higher magnesium filler is acceptable.
Everything above assumes clean material. Aluminum oxide, oil, and — critically — embedded iron particles from shared tooling are the root causes of most weld and coating failures. Dedicated stainless brushes and separate handling from carbon steel are not optional. The filler choice is covered in more detail in our aluminum welding wire guide.
Forming, Machining, and Finishing
Forming is best in O and workable in H32, with bend radii that must open up as temper hardness rises. 5086 is generally a little more forgiving than 5083 in complex forming, which is one of the reasons it gets specified for superstructures and tank work. Expect more springback than 5052 and plan the bend allowance accordingly.
Machining rates fair to good. Harder tempers (H32, H34) cut more cleanly with better chip breakage than soft O material, which tends to be gummy. Carbide tooling, positive rake geometry, and generous cutting fluid are the standard recommendations. It is not in the same class as 6061 or 2011, and shops quoting against free-machining alloys will notice the difference.
Anodizing works, but functionally rather than decoratively. 5086 anodizes to a harder, more protective surface; it does not give the bright, uniform appearance of 5005 or 6063, and the higher magnesium content makes color match across batches harder to hold. Specify it for protection, not for appearance. Our anodizing quality guide covers where these finishes go wrong.
Where 5086 Is Used
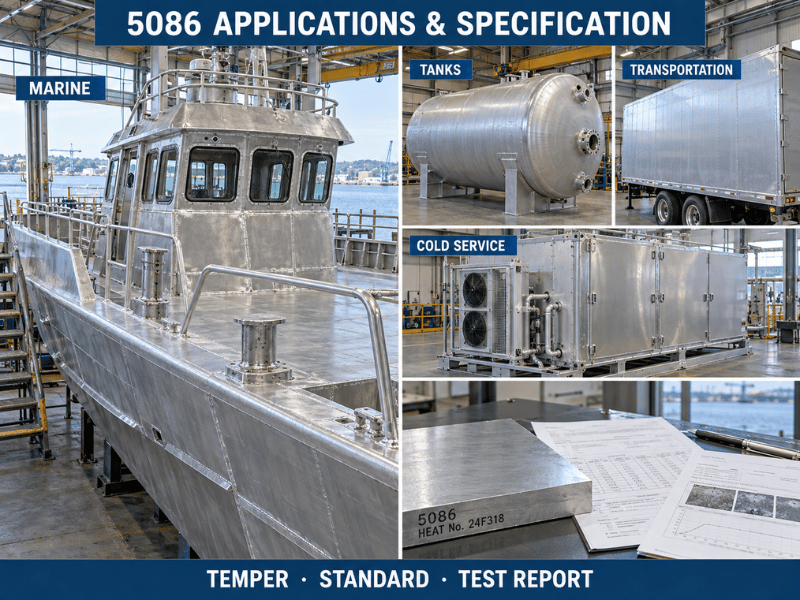
Marine and shipbuilding is the anchor application: hull plating on small and mid-size craft, decks, bulkheads, superstructures, gangways, masts, and fuel and water tanks. 5083 tends to win the immersed lower hull; 5086 wins the upper structure, where there is more forming and more welding and less hydrostatic load.
Pressure vessels and tanks — 5086 is a standard material for unfired welded pressure vessels under ASME Section VIII, and for road tankers carrying fuel, water, and a range of chemicals that do not attack aluminum. Its low-temperature behavior matters here: unlike carbon steel, it has no ductile-to-brittle transition, and it retains toughness down to cryogenic temperatures, which is why it appears in LNG-adjacent and refrigerated service.
Transportation covers truck and trailer bodies, tipper bodies, rail car panels, and vehicle armor. The H131 temper of 5086 is qualified to MIL-DTL-46027 for light armored vehicles — a niche but real specification that few other 5xxx alloys carry.
Other structural work includes drilling rig components, coastal construction, TV and transmission towers, and cryogenic or non-magnetic equipment housings, where the alloy’s non-magnetic nature is a functional requirement rather than a bonus.
5086 vs 5083, 5052, and 6061
5083 and 5086 are frequently quoted interchangeably, and they are not. The difference is about 10–15% of strength traded against formability, weldability, and cost.
| Property | 5086 | 5083 | 5052 | 6061 |
|---|---|---|---|---|
| Main alloying | Mg 3.5–4.5%, Mn 0.2–0.7% | Mg 4.0–4.9%, Mn 0.4–1.0% | Mg 2.2–2.8% | Mg 0.8–1.2%, Si 0.4–0.8% |
| Tensile (MPa, typical) | 275 – 345 (H32) | 300 – 350 (H32) | 210 – 260 (H32) | ~310 (T6) |
| Yield (MPa, typical) | 195 – 240 (H32) | 215 – 260 (H32) | 160 – 195 (H32) | ~275 (T6) |
| Elongation (%) | 6 – 12 | 10 – 14 | 12 – 20 | 8 – 12 |
| Density (g/cm³) | 2.66 | 2.66 | 2.68 | 2.70 |
| Thermal conductivity (W/m·K) | 117 – 127 | 117 – 121 | ~138 | ~167 |
| Heat treatable | No | No | No | Yes |
| Marine corrosion | Excellent | Excellent | Good | Moderate |
| Relative cost vs 5052 | Moderate premium | Higher premium | Baseline | Lower |
Choosing between 5086 and 5083 is usually a single question: is strength or fabrication the binding constraint?
- Pick 5083 where strength governs — immersed hull plating, primary offshore structure, cryogenic service, pressure vessels where higher ASME allowable stress lets you thin the wall, or anywhere a classification society wants maximum margin. Full data is in our 5083 aluminum guide.
- Pick 5086 where fabrication governs — welded superstructures and tanks, parts that need tighter bends than 5083 tolerates, secondary structure, or a project where 5083’s premium buys strength the design will not use.
The common answer on larger vessels is both: 5083-H116 below the waterline, 5086-H116 for upper hull and decks, 5086-H32 for dry interior structure. That combination typically lands several percent below an all-5083 build without giving up anything in service.
5052 is the choice when neither strength nor marine certification is required and formability or cost leads — see the 5052 aluminum guide. 6061 wins when the part is machined rather than welded and needs heat-treatable strength; its welded strength and seawater performance are both worse than 5086’s. Details in the 6061 aluminum guide.
When 5086 Is the Wrong Choice
The conditions matter more than the application labels, so this is written as conditions rather than a list of parts.
Specify 5086 when:
- The structure is welded and sees seawater or marine atmosphere, and H116 or H321 is on the order.
- The part needs more formability than 5083 allows while keeping marine-grade corrosion performance.
- The design is strength-adequate at 5086 levels and the 5083 premium buys nothing.
- Service temperature stays below 65 °C, or the warm zones are isolated.
- Low-temperature toughness is required — cryogenic or refrigerated service where carbon steel would go brittle.
Look elsewhere when:
- Sustained service exceeds ~65 °C in a corrosive environment. Beta-phase sensitization is not recoverable; use 5052 or 6061.
- Decorative anodizing is the finish. 5086 anodizes protectively, not attractively — 5005 or 6063 is the right call.
- The part is primarily machined from solid at high volume. 6061 or 2011 will run faster and cheaper.
- Peak strength is the requirement and welding is minimal. 6061-T6 or 7075-T651 outperforms any 5xxx alloy.
- The assembly couples 5086 to steel or copper alloys without isolation and without sacrificial protection. Galvanic attack will be the failure mode.
Across the 5xxx family as a whole, the marine grade aluminum overview covers how 5052, 5083, and 5086 divide the applications between them.
Standards, Equivalents, and Documentation
| Standard | Scope |
|---|---|
| ASTM B209 | Aluminum and aluminum-alloy sheet and plate |
| ASTM B928/B928M | High-magnesium sheet and plate for marine service (defines H116 / H321) |
| ASTM B221 | Extruded bar, rod, wire, profiles, and tube |
| ASTM B210 / B241 | Seamless and welded tube and pipe |
| ASME SB-209 | Pressure-vessel use of 5086 sheet and plate |
| AWS A5.10 / D1.2 | Filler metal classification and structural weld design |
| EN 485 / EN 573 | European sheet, strip, plate and composition requirements |
| MIL-DTL-46027 | Armor-grade 5086 (H131) |
Equivalent designations: UNS A95086, EN AW-5086, AlMg4, Werkstoff 3.3545, ISO AlMg4.
For procurement, three documents carry the weight. A mill test certificate (MTC) to EN 10204 3.1 should be standard on every order — it ties the mechanical values and the heat number to the material in your hands. ASTM B928 ordering requires the exfoliation and intergranular corrosion test results, not just a statement of compliance. Third-party inspection (SGS or equivalent) is worth adding when the material is going into classified marine structure. Classification society approvals (DNV, ABS, LR, CCS) are arranged per project rather than held generically — raise it early with your yard, because approval lead time is usually longer than material lead time.
Practical notes for the purchase order: state the temper explicitly, state the governing standard (B209 or B928 — they are not interchangeable), state thickness and tolerance rather than a nominal gauge, name the surface and any protective film, and attach the test requirements. Most 5086 problems are specification problems, not metallurgy problems.
Working With Linsy Aluminum
Linsy Aluminum supplies 5086 aluminum as plate and sheet in O, H111, H112, H32, H34, H116, and H321, and as bar in H111 and H112 — bar is not produced in the marine tempers, since H116 and H321 are flat-rolled specifications. In-house capability covers CNC machining, welding, laser cutting, and surface finishing; forging is coordinated through partner process facilities rather than run in-house, so allow for it in planning if your part needs it.
Every shipment carries a mill test certificate (MTC), and SGS testing can be arranged on request. We do not issue classification-society certificates as standard — where DNV, ABS, LR, or CCS approval is required, confirm it with your yard early and we will work to the project’s approval path. For non-stock dimensions, typical lead time is 10–60 days, and we support low minimum order quantities on trial and prototype builds.
Send your drawing or specification and we will confirm available tempers, sizes, tolerances, and documentation, and flag anything in the service conditions that points to a different alloy.
Conclusion
5086 earns its place as the practical middle of the marine 5xxx range: more strength than 5052, more formability and weldability than 5083, and excellent seawater corrosion in the tempers that are tested for it. The three things that decide whether it is right for a job are the temper on the order, the 65 °C ceiling, and how the welded joint is designed around HAZ softening. Get those right and 5086 is a forgiving, well-documented alloy with decades of service behind it. Get them wrong — H32 specified for immersed service, sustained warm operation, or a weld sized on parent-metal strength — and the failure will look like a material problem when it was a specification problem.
Frequently Asked Questions
Is 5086 stronger than 5083?
No. 5083 carries roughly 10–15% more tensile and yield strength because of its higher magnesium range (4.0–4.9% versus 3.5–4.5%). 5086 trades that margin for better formability, easier welding, and usually lower material cost. Where the design does not need 5083’s extra strength, 5086 is the more economical call.
What is the 65 °C limit on 5086?
Sustained service above about 65 °C (150 °F) can cause magnesium to precipitate at grain boundaries as the beta phase (Al₃Mg₂), which is anodic to the surrounding metal and opens the alloy to intergranular corrosion, exfoliation, and stress corrosion cracking. The change is not reversible by heat treatment. H116 and H321 tempers are processed and tested to resist it, but the temperature ceiling still applies.
Does 5086 lose strength when welded?
Yes, in the heat-affected zone. 5086 is non-heat-treatable, so the welding cycle anneals out the cold work locally and the HAZ reverts toward the O condition — an H32 assembly retains roughly 70–75% of parent yield strength across that band, with yield falling from ~210–230 MPa toward ~115–145 MPa. Welded structure should be sized on annealed HAZ properties per AWS D1.2, not on parent-temper values.
Which filler wire should I use for 5086?
ER5183 is the usual first choice for welding 5086 to itself, giving the closest strength match to the base metal with good marine corrosion behavior. ER5356 is the general-purpose alternative and is slightly lower in as-welded strength. ER5556 is specified where joint strength governs and a higher-magnesium filler is acceptable.
Is 5086 suitable for pressure vessels?
Yes. 5086 is a standard material for unfired welded pressure vessels under ASME Section VIII, supplied to ASME SB-209, and it is widely used for road tankers and chemical storage tanks. It has no ductile-to-brittle transition, so it also performs well at low temperatures. 5083 is preferred where higher allowable stress permits a thinner wall.
Can 5086 be anodized?
Yes, but for protection rather than appearance. It anodizes to a harder, more corrosion-resistant surface, but the high magnesium content makes the finish less bright and uniform than 5005 or 6063, and color consistency across batches is harder to hold. For decorative anodized parts, specify 5005 or 6063 instead.






