


What Is 5005 Aluminum?
5005 is the lean-magnesium end of the 5xxx family, carrying roughly 0.8% magnesium — well below 5052 (~2.5%) or 5083 (~4.5%). That single number explains almost everything about it. With less magnesium, 5005 trades the high strength of its 5xxx cousins for two things buyers actually specify it for: an excellent anodizing response and corrosion resistance close to 3003’s at a lower weight of alloying content. It is the standard choice for anodized architectural sheet, and its mechanical properties sit in the same band as 3003 rather than in structural territory.
It is a non-heat-treatable alloy. Every increment of strength comes from cold work, expressed in the H-tempers, and it cannot be precipitation-hardened the way 6061 or 7075 can. The practical consequence is that hardness and strength are set by the temper you buy, not by anything you do to the part afterwards — except annealing it back down.
There is also a genuine advantage that gets overlooked: because 5005 sits well under the ~3% magnesium threshold, it is not prone to the β-phase (Al₃Mg₂) grain-boundary precipitation that limits higher-magnesium grades such as 5083 and 5056 to roughly 65 °C in sustained service. For warm, mildly corrosive duty, 5005 does not carry that constraint.
5005 Chemical Composition
Composition limits per ASTM B209 / EN 573-3, in weight percent. Magnesium is the only deliberate alloying element of consequence; everything else is either a small controlled addition or an impurity ceiling.
| Element | Content (%) | Role |
|---|---|---|
| Magnesium (Mg) | 0.50 – 1.10 | Primary alloying element; strength and corrosion behaviour |
| Silicon (Si) | 0.30 max | Impurity, kept low for anodizing clarity |
| Iron (Fe) | 0.70 max | Impurity; affects surface finish |
| Copper (Cu) | 0.20 max | Kept low to protect corrosion resistance and anodic colour |
| Manganese (Mn) | 0.20 max | Minor addition, grain structure |
| Chromium (Cr) | 0.10 max | Minor corrosion-resistance addition |
| Zinc (Zn) | 0.25 max | Trace |
| Titanium (Ti) | 0.05 – 0.15 | Grain refiner |
| Others (each) | 0.05 max | Trace impurities |
| Others (total) | 0.15 max | Sum of trace impurities |
| Aluminium (Al) | Remainder | Base |
The tight ceilings on copper and silicon matter more than they look. Both elements discolour an anodic film — copper pushes it toward yellow, silicon toward grey — which is why low-Cu, low-Si chemistry is what makes 5005 an anodizing alloy rather than just another 5xxx grade.
5005 Hardness by Temper
Hardness is where 5005’s cold-worked structure shows up most directly. Values below are typical Brinell figures measured with a 500 kg load and 10 mm ball (ASTM E10), the convention used for wrought aluminium.
| Temper | Condition | Brinell Hardness (HB) | Approx. shear strength (MPa) |
|---|---|---|---|
| O | Annealed | 28 | 76 |
| H32 | Strain hardened, stabilised (¼ hard) | 36 | 96 |
| H34 | Strain hardened, stabilised (½ hard) | 41 | 96 |
| H36 | Strain hardened, stabilised (¾ hard) | 46 | 103 |
| H38 | Strain hardened, stabilised (full hard) | 51 | 110 |
Three things follow from that table.
The range is narrow. Across the entire temper span 5005 moves from 28 to 51 HB — under double from annealed to full hard. Compare that with 6061, which roughly triples from O to T6. If your design needs hardness that cold work cannot deliver, 5005 is the wrong starting point and no amount of temper selection will fix it.
Hardness is a receiving-inspection tool, not a design input. HB is fast and non-destructive enough to check a delivery against its MTC, and it correlates well with tensile strength. But no engineer sizes a bracket off Brinell. Use HB to confirm you received the temper you ordered; use tensile and yield for the actual calculation.
Anodizing changes surface hardness, not bulk hardness. This is the most common misunderstanding in a hardness enquiry. The anodic oxide layer is far harder than the substrate — aluminium oxide sits well above any aluminium alloy on the hardness scale — so scratch and wear resistance improve substantially. The underlying metal is unchanged, and a 5005-H34 panel still has 41 HB beneath its coating. If a drawing says “harder”, establish whether it means surface wear resistance (anodize it) or load-bearing capacity (change alloy).
5005 Mechanical Properties by Temper
Typical values for sheet and plate. Note that ASTM B209 minimum values sit below these figures and vary with thickness — guaranteed numbers for your specific lot come from the MTC, not from this table.
| Temper | Tensile strength (MPa) | Yield strength (MPa) | Elongation (% in 50 mm) | Hardness (HB) |
|---|---|---|---|---|
| O | 124 | 41 | 25 | 28 |
| H32 | 138 | 117 | 11 | 36 |
| H34 | 159 | 138 | 8 | 41 |
| H36 | 179 | 165 | 6 | 46 |
| H38 | 200 | 186 | 6 | 51 |
The elongation column is the one that decides most real specifications. Dropping from H32 to H38 buys roughly 45% more tensile strength and costs you nearly half the available elongation — 11% down to 6%. For a flat decorative panel that trade is free. For anything with a formed radius, a hem, or a rolled edge, H32 or H34 is the ceiling, and O is the answer when the forming is severe.
The H1x and H3x designations are not interchangeable. H1x tempers are strain hardened only; H3x tempers are strain hardened and then stabilised with a low-temperature thermal treatment, which trims a little strength and returns meaningful ductility. That stabilisation is why H32/H34 dominate architectural work — the extra ductility buys formability, and the stabilised condition holds its properties instead of age-softening on the shelf.
5005 Physical Properties
| Property | Value |
|---|---|
| Density | 2.70 g/cm³ |
| Melting range | 632 – 655 °C |
| Thermal conductivity | ~201 W/m·K (O temper) |
| Electrical conductivity | ~52% IACS (decreases in harder tempers) |
| Coefficient of thermal expansion | 23.7 × 10⁻⁶ /°C (20–100 °C) |
| Specific heat capacity | ~900 J/kg·K |
| Modulus of elasticity | ~69 GPa |
| Poisson’s ratio | 0.33 |
Two of these carry purchasing weight. Thermal and electrical conductivity at ~201 W/m·K and ~52% IACS are high for a 5xxx alloy — the low magnesium content is why — and both fall off as temper hardness rises, so a conductivity-driven specification should be placed against the O or H32 condition rather than assumed across the range. Melting range matters mainly for welding and any elevated-temperature service discussion.
Corrosion Resistance and Anodizing
Atmospheric and mildly alkaline service. 5005 resists general atmospheric corrosion comparably to 3003, including industrial and coastal atmospheres, with the added 5xxx advantage of better performance in slightly alkaline conditions. It is not the choice for continuous seawater immersion — 5083 and 5086 hold that ground — but for marine atmosphere, coastal architecture, and interior boat hardware it is comfortably adequate.
The 65 °C question. Higher-magnesium 5xxx grades carry a sustained-service ceiling near 65 °C, above which β-phase precipitation along grain boundaries opens a stress-corrosion-cracking path. At ~0.8% Mg, 5005 is below the threshold where that mechanism is a practical concern. This is a real differentiator against 5083 and 5056 in warm service, and it is one of the least-appreciated reasons to pick it.
Elevated temperature still softens it. Cold-worked tempers lose strength progressively as service temperature rises, with full annealing around 345 °C. If a part will see sustained heat, design against the annealed (O-temper) values rather than the H-temper values on the order — the cold work you paid for does not survive the heat.
Anodizing — and the catch. When anodized, 5005 produces a clear, homogeneous film that is more transparent than 3003’s and gives an excellent colour match to 6063 architectural extrusions. That combination is why it is the default for anodized façades and decorative trim.
The catch: 5005 can anodize with visible streaking, sometimes called “barcoding”. If the finish is critical — a façade panel in full view, a large uninterrupted surface — specify 5005-AQ (anodising quality, sometimes sold as special anodising quality) at the time of order. It costs more and it is far cheaper than discovering the streaks after installation. Galvanic corrosion is the other standing caveat: like any aluminium, 5005 corrodes rapidly when electrically coupled to a more noble metal in a wet environment, so isolate it from steel and copper alloys.
Working With 5005
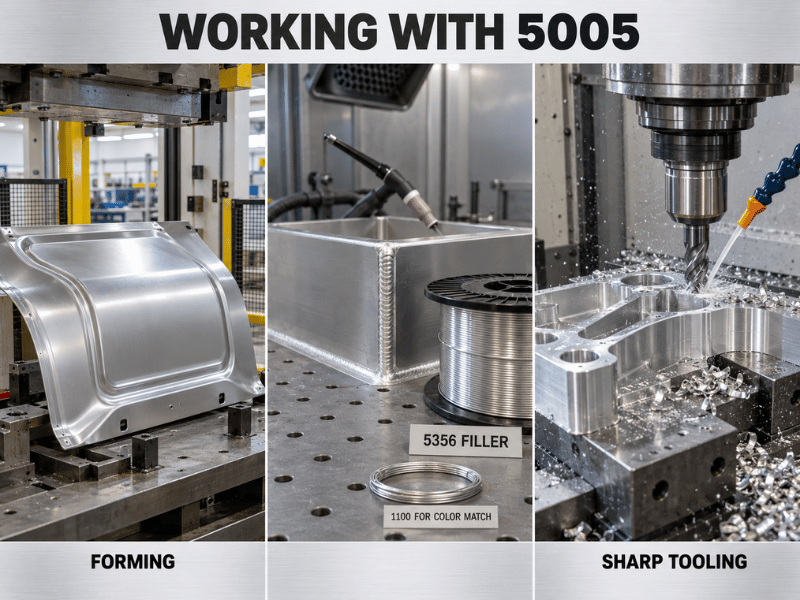
Forming. 5005 forms readily, especially annealed. Thin H32 sheet can be bent to very tight radii — roughly 0 to ½ × thickness — without failure, and H34 generally manages 1 to 2 × thickness. Deep drawing, spinning, and roll forming are standard in the O condition. Forming loads and tool wear are lower than for carbon steel on comparable geometry.
Welding. GTAW (TIG) and GMAW (MIG) both run cleanly, as does resistance spot welding and friction stir welding. Filler choice splits by priority: 4043 (Al-Si) is often preferred for its hot-cracking tolerance and weld-bead fluidity, while 5356 (Al-Mg) produces mechanically stronger weld metal. Neither requires pre- or post-weld heat treatment, and the low magnesium content means there is no meaningful post-weld sensitization risk. Expect the heat-affected zone to revert toward annealed strength — as with every non-heat-treatable alloy, that strength is not coming back.
Machining. Fair. 5005 machines better than very soft grades such as 1100 or 3003 and less well than free-cutting alloys such as 2017 or 6082. Its softness produces gummy chips and built-up edge, so use sharp tooling, higher cutting speeds, and generous lubrication. Where a part is machining-dominated rather than finish-dominated, 6061 is the better call.
Annealing. Standard treatment is around 345 °C followed by slow cooling. It is not generally hot worked — forging is rarely applied to 5xxx alloys and is not a normal route for 5005.
5005 vs 3003 vs 5052 vs 6061
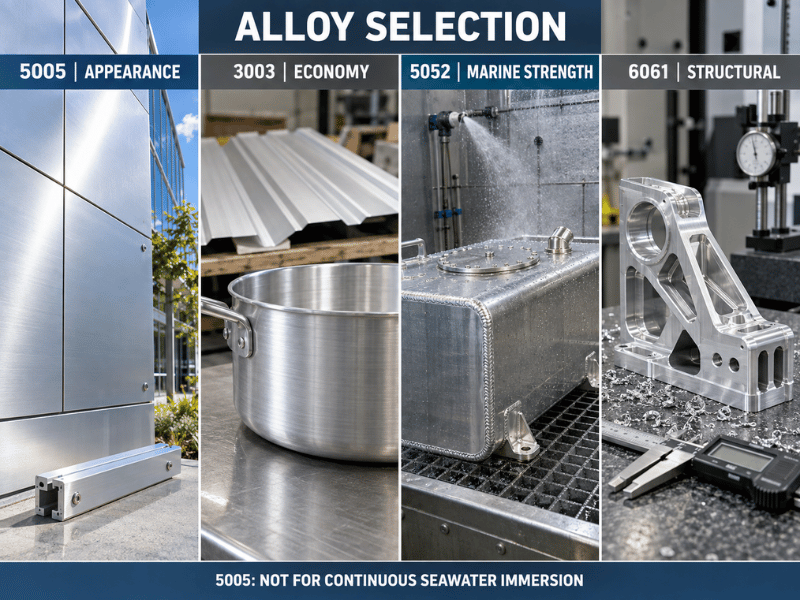
| Alloy and temper | Tensile (MPa) | Yield (MPa) | Elongation (%) | Hardness (HB) | Anodizing | Best for |
|---|---|---|---|---|---|---|
| 5005-H34 | 159 | 138 | 8 | 41 | Excellent — clear film, matches 6063 | Anodized architectural panels, signage |
| 3003-H14 | 152 | 145 | 8–16 | 40 | Good — may discolour slightly | Cookware, roofing, general sheet metal |
| 5052-H32 | 228 | 193 | 12 | 60 | Fair — less uniform | Marine parts, fuel tanks, formed enclosures |
| 6061-T6 | 310 | 276 | 12 | 95 | Good — slightly less uniform | Structural frames, extrusions, machined parts |
5005 vs 3003. At comparable temper these two are close on strength — within a few percent — so anyone choosing between them on strength is optimising the wrong variable. 5005 wins on anodizing clarity, colour match to 6063, and conductivity (~52% IACS against ~40%). 3003 wins on price and marginally better deep-drawing. Pick 5005 when the surface is visible; pick 3003 when it isn’t.
5005 vs 5052. 5052 is substantially stronger — 228 MPa against 159 MPa at the temper most people actually buy — and holds up better in true marine immersion. It pays for that with a less uniform anodic film and higher cost. 5052 for structure and saltwater; 5005 for appearance.
5005 vs 6061. Different categories. 6061-T6 roughly doubles 5005’s yield strength and machines far better, but it is heat-treatable, loses formability in T6, and its copper content costs some corrosion resistance and anodic uniformity. 5005 is a decorative sheet alloy; 6061 is a structural alloy.
Go/No-Go: When to Specify 5005
Specify 5005 when:
- The part will be anodized and appearance is an acceptance criterion — especially where it must colour-match 6063 extrusions
- The environment is atmospheric, coastal, or mildly alkaline rather than continuous immersion
- The part is formed, bent, or drawn, and moderate strength is sufficient
- Service temperature is ambient or only moderately elevated, and you want to avoid the 65 °C sensitization limit that constrains higher-Mg grades
- Higher thermal or electrical conductivity than 5052/5083 is useful
Look elsewhere when:
- Load-bearing capacity drives the design — go to 5052 for formed sheet or 6061-T6 for structure
- The part is submerged or in splash-zone marine service — 5083 or 5086
- Machining volume is high and cycle time matters — 6061
- Wear resistance is the requirement in bulk — anodizing improves the surface only, and a 4xxx or hard-coated solution may be needed
- The specification calls for hardness above roughly 51 HB, which is where 5005 stops
Where 5005 Is Used
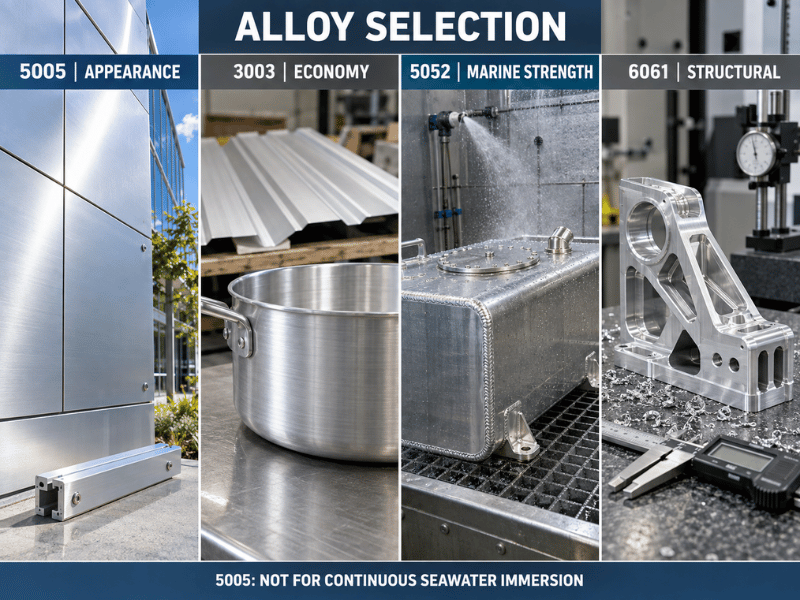
| Sector | Typical parts | Why 5005 |
|---|---|---|
| Architecture and construction | Facades, roofing, wall panels, decorative trim, anodized profiles | Anodizing clarity, corrosion resistance, colour match to 6063 |
| Signage and display | Anodized signs, nameplates, retail displays, decorative panels | Bright uniform finish, formability, light weight |
| Marine and coastal | Interior boat fittings, marine hardware, coastal architectural parts | Atmospheric marine corrosion resistance without immersion-grade cost |
| Electrical | Busbars, conductor rail, enclosures | ~52% IACS conductivity with formability |
| Appliance and consumer | Appliance trim, utensils, furniture, packaging | Formed-and-anodized economics |
| Automotive and transport | Interior trim, non-structural panels | Formability and finish quality |
| Chemical and process | Tank panels, equipment housings | Alkaline resistance and weldability |
Pros and Limitations at a Glance
| Dimension | Advantage | Watch-out |
|---|---|---|
| Anodizing | Clear, uniform film; best-in-class 6063 colour match | Streaking possible — specify 5005-AQ for critical finishes |
| Corrosion | Excellent atmospheric and coastal | Not for continuous seawater immersion |
| Temperature safety | Below the 3% Mg threshold — no 65 °C SCC ceiling | Cold-worked tempers still soften with sustained heat |
| Formability | Excellent in O; tight bend radii in H32/H34 | Ductility falls fast by H36/H38 |
| Weldability | Clean TIG/MIG, no pre- or post-heat, no sensitization risk | HAZ reverts toward annealed strength |
| Machining | Better than 1100/3003 | Gummy chips; well behind 6061 |
| Conductivity | ~201 W/m·K, ~52% IACS — high for 5xxx | Both drop in harder tempers |
| Strength | Adequate for decorative and light-duty work | Ceiling around 200 MPa / 51 HB |
Conclusion
5005 earns its place on a drawing for one reason: it anodizes better than the alternatives at a price that makes decorative architectural work economical — while matching 3003 on corrosion resistance and dodging the elevated-temperature sensitization limit that bites higher-magnesium 5xxx grades. Its hardness window is narrow by design (28 HB annealed to 51 HB full hard), and the temper choice is where specs live or die: H32/H34 for formed parts, H38 only when nothing forms, and 5052 or 6061 the moment load-bearing, immersion service, or machining volume becomes the driver. If the surface is visible and exposed, spend the small premium on 5005-AQ.
At Linsy Aluminum, we supply 5005 across sheet, coil, plate, bar, tube, and wire in the common tempers, with in-house machining, welding, laser cutting, anodizing, and polishing. Send your drawing and spec — temper and anodizing requirement included — and we’ll confirm hardness and finish before you commit.
Frequently Asked Questions
How hard is 5005 aluminum?
It depends entirely on temper, because 5005 is non-heat-treatable and gains hardness only from cold work. Typical Brinell values run 28 HB in the annealed O condition, 36 HB in H32, 41 HB in H34, 46 HB in H36, and 51 HB in H38. Published figures vary somewhat by source and thickness, so treat these as typical and confirm guaranteed values on the MTC.
Is 5005 aluminum heat treatable?
No. 5005 cannot be precipitation-hardened; all strength comes from strain hardening, expressed in the H-tempers. It can be annealed — around 345 °C followed by slow cooling — but that softens it rather than strengthening it. If you need heat-treatable strength, 6061 is the usual move.
Which 5005 temper should I specify?
Use O when the part is deeply drawn or severely formed. H32 is the general-purpose choice and the safest default for architectural sheet, with H34 adding strength where some formability can be given up. H36 and H38 deliver maximum strength but elongation drops to around 6%, which rules out most forming. H32 and H34 are preferred for anodized architectural work because the stabilised H3x condition holds its properties.
Does anodizing make 5005 harder?
It hardens the surface, not the metal. The anodic oxide layer is considerably harder than the aluminium substrate, so scratch and wear resistance improve substantially — but the bulk hardness underneath is unchanged, and a 5005-H34 part still has 41 HB below its coating. Anodizing is the right answer for surface durability and the wrong answer for load-bearing capacity.
Is 5005 suitable for marine environments?
For marine atmosphere, yes — it performs well in coastal and salt-spray exposure and is widely used for interior boat fittings and coastal architectural parts. For continuous seawater immersion or heavily loaded marine structure, higher-magnesium grades such as 5083 or 5086 are the correct specification. 5005 also has an advantage here: at ~0.8% Mg it sits below the threshold where the 65 °C sensitization and stress-corrosion-cracking limit applies to grades like 5083 and 5056.






