


5053 aluminum is an Al-Mg sheet and plate grade carrying roughly 3.5% magnesium. It has a registered chemistry but no current row in the ASTM B209 table of sheet and plate grades, so what it does not have is a guaranteed tensile minimum you can design against. That single fact decides how the grade has to be bought.
The magnesium range sits between 5052 and 5083, which is where its strength and its saltwater behaviour come from, and it inherits the 65 °C service ceiling that every alloy above 3% Mg carries. What it also carries is a paperwork problem no other 5xxx grade has: the certificate is the only place its numbers exist.
What 5053 Is and What the Standard Does Not Fix
5053 is a non-heat-treatable aluminum-magnesium alloy. Its composition limits are registered with the Aluminum Association, so the number has a fixed meaning and the grade is real. What 5053 does not have is a row in the current ASTM B209 table of sheet and plate grades, and that is the part that matters at the point of purchase.
No B209 row means no standard temper ladder for the grade and no published tensile, yield or elongation minimum. There is also no EN 573-3 designation to cross-reference, and the nearest active European registration for this composition band is EN AW-5754, or AlMg3.
None of that makes the metal unusable. It moves the guarantee from the standard to the mill: the heat you receive is what the certificate says it is. An order for 5053 is only as strong as the MTC that travels with it, and that is the document to negotiate over before price.
Registered Chemistry: Read the Iron Line First
The registered limits for 5053 are narrow, and the narrowest of them is the one buyers skip.
| Element | 5053 (registered) | 5052 | 5754 | 5083 |
|---|---|---|---|---|
| Magnesium | 3.1–3.9 | 2.2–2.8 | 2.6–3.6 | 4.0–4.9 |
| Manganese | 0.03–0.10 | ≤0.10 | ≤0.50 | 0.40–1.0 |
| Iron + Silicon | ≤0.03 combined | Fe ≤0.40, Si ≤0.25 | Fe ≤0.40, Si ≤0.40 | Fe ≤0.40, Si ≤0.40 |
| Copper | 0.03–0.10 | ≤0.10 | ≤0.10 | ≤0.10 |
| Chromium | — | 0.15–0.35 | ≤0.30 | 0.05–0.25 |
| Titanium | ≤0.02 | — | ≤0.15 | ≤0.15 |
| Basis | AA wrought composition register | ASTM B209 | ASTM B209 | ASTM B209 |
Read the iron line before anything else. The registered limits hold iron and silicon to 0.03% combined, more than ten times tighter than the 5xxx sheet grades in B209, so a certificate showing 0.25% Fe is describing a different composition — not necessarily a defective one, but not the registered alloy either. Fix the chemistry limits in writing before the order rather than arguing over the certificate after delivery.
Strength on This Grade Comes From the Certificate
Strength in this alloy is solid-solution strengthening from magnesium plus strain hardening from cold work. There is no precipitation hardening, so there is no heat treatment that raises it and no aging curve to wait on.
| Grade and temper | Minimum tensile | Minimum yield | Source of the minimum |
|---|---|---|---|
| 5052-H32 | 215 MPa | 160 MPa | ASTM B209 |
| 5053-H32 | None published | None published | Mill certificate for the heat |
| 5083-H116 | 305 MPa | 215 MPa | ASTM B928 |
Use the two ends of that table as brackets, not as a 5053 value. The grade inherits the chemistry between them, not either minimum, so a quotation that quotes you 5052’s figures is quoting a different alloy. Ask for tensile, yield and elongation on the certificate and check them against the datasheet you approved before the order went in.
Sizing a part before a certificate exists is the awkward case. Design to the 5052-H32 minimum and treat whatever the 5053 heat delivers as margin; that keeps the calculation conservative and avoids resting it on a number nobody has published.
Tempers You Can Actually Buy
The H system describes what was done to the metal. H1x is strain hardened only, H2x is strain hardened and then partially annealed, and H3x is strain hardened and stabilized against natural aging.
On a 5xxx rolling route the usable supply states are O, H32, H34 and H111 for sheet, and O and H112 for plate. Full-hard tempers exist in the system but stop earning their money here: the extra proof strength is real, and it vanishes next to a weld, because the heat-affected zone anneals back toward O no matter which hard temper you bought. On a part that gets formed, the same hardness leaves too little elongation to work with.
H116 and H321 deserve a separate warning. Both are marine plate tempers defined inside ASTM B928, and both are tied to a corrosion test rather than to strength alone. They were written for the high-magnesium marine grades, and 5053 has no B928 row, so 5053-H116 is not something you can buy against a standard.
Welding 5053: Filler Choice and the Soft Zone
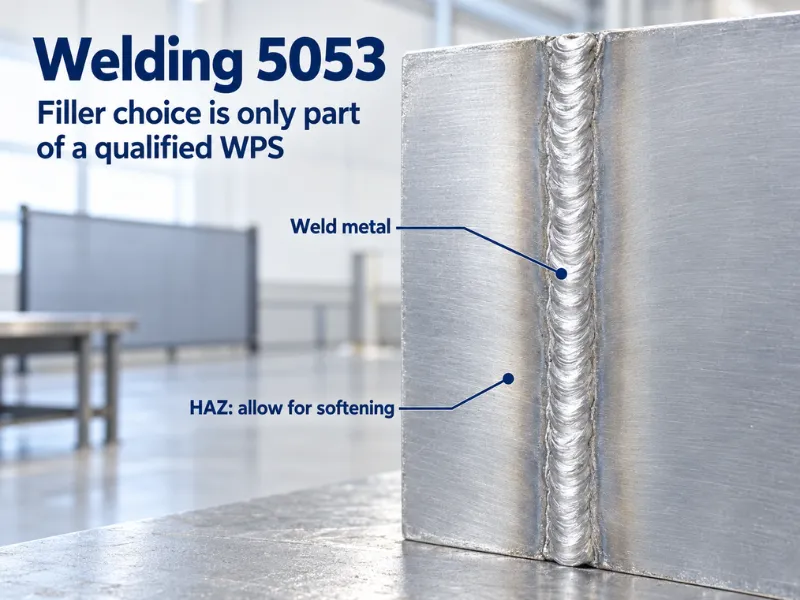
5053 welds readily with GTAW and GMAW, and the filler decision is settled by the magnesium content rather than by preference. Use ER5356 as the default, or ER5183 where the joint needs the highest as-welded strength.
Do not weld this alloy with a 4xxx filler. Above roughly 3% magnesium the aluminium-silicon fillers promote eutectic melting and give poor as-welded properties, which is why 5052 is generally treated as the upper limit for 4043 and everything above it takes a 5xxx filler.
The heat-affected zone is the design problem, not the weld itself. Welding anneals the parent metal next to the bead back toward O condition, so proof strength there drops to the annealed level and stays there. Being non-heat-treatable, the alloy has no aging response to restore it, and a full re-solution treatment is not a workshop option. Locate seams away from peak stress and design the joint on annealed properties.
Keep interpass temperature down and skip preheat; the alloy conducts heat away fast enough that preheat mostly buys distortion. One more limit travels with the filler: ER5356 and ER5183 are both above 3% Mg, so the weld metal shares the base metal’s high-temperature ceiling. Where the joint runs hot, ER5554 keeps the deposit under the line at some cost in joint strength.
The 65 °C Line
Above about 65 °C, alloys with more than 3% magnesium progressively precipitate the beta phase (Al3Mg2) along grain boundaries. The result is a sensitized microstructure that loses resistance to intergranular attack and to stress corrosion cracking, and it does not recover if the part later runs cool again.
5053 sits on the wrong side of that line across its whole registered range, because the magnesium floor is 3.1%. This is not a question of a bad heat or a hot summer; every 5053 is above the threshold by definition.
The condition is measurable rather than theoretical. ASTM G67 measures mass loss after nitric acid exposure, and marine plate is normally accepted at 15 mg/cm² or below. That test is written into the B928 tempers, which is the practical consequence: the grade that can prove it is sensitization-resistant is 5083-H116 or 5083-H321, not 5053.
Where the service temperature is unavoidable, the answer is less magnesium rather than more. 5454 at 2.4–3.0% Mg and 5052 at 2.2–2.8% are both under the threshold. Exhaust-adjacent parts, steam and hot chemical service are the wrong application for this grade, and the same applies to its weld metal.
Forming and Bend Radius
Magnesium raises the work-hardening rate, so 5053 hardens faster than 5052 at the same amount of cold work. In practice that means more springback, less remaining ductility, and a shorter forming window for any given temper.
Form in O or H32 and you have room to work. H34 is a panel and cladding temper and will take a gentle curve, not a sharp one. Anything harder is a flat-part temper.
On bend radius, be sceptical of published tables. Radii quoted for 5052 do not transfer, because the alloy work-hardens differently, and there is no B209 table for 5053 to fall back on. Prove the radius with a bend test on the actual heat at the temper you will run, and write the result into the purchase specification.
Corrosion and Finishing
In seawater and marine atmosphere 5053 performs well, and better than 5052 on pitting resistance because the magnesium level is higher. It is not the equal of 5083, which carries more magnesium plus manganese and chromium, and it should not be sold as a substitute where 5083 was specified for immersion.
General industrial and fresh-water exposure gives no trouble. Where the assembly mixes metals, isolate the aluminium from steel fasteners and from stainless, or the joint will corrode regardless of which 5xxx grade you chose.
Anodizing is the weak point. Magnesium is what limits finish quality on this family, producing a darker and less uniform coating than a 6xxx alloy, and a low-iron heat does not remove that effect. If the face is visible and anodized, specify 5005 or 6063. If the part is 5053, paint it, and treat the surface before painting rather than relying on the mill finish.
5053 Against 5052, 5754 and 5083
| Grade | Magnesium | Standard position | What it decides |
|---|---|---|---|
| 5052 | 2.2–2.8 | Full B209 row, O to H38 | Cheapest route to a guaranteed minimum; adequate for most sheet work |
| 5754 | 2.6–3.6 | Full B209 and EN 573-3 row | The same composition band with a standard behind it |
| 5053 | 3.1–3.9 | Registered, no B209 row | Composition is fixed; the certificate decides the numbers |
| 5083 | 4.0–4.9 | B209, plus B928 marine tempers | The marine and cryogenic grade with a certified corrosion temper |
The comparison that matters is with 5754 aluminum, not with 5083: the two share a composition band, and 5754 is the version of it that carries an active registration, published property limits and an EN designation. 5083 differs from 5053 by more than magnesium, adding manganese and chromium along with the B928 marine tempers. 5052 sits about a point lower on magnesium, which shows up as a modest strength step rather than a different class of alloy.
Go / No-Go: Where 5053 Stops Working
Go when the specification already calls for 5053 and the paperwork can be enforced. Re-qualifying a drawing to 5754 usually costs more than buying 5053 properly, and in that situation the grade covers marine and industrial fabrication, fuel tanks, chemical and process vessels, truck bodies and welded assemblies, all at service temperatures under 65 °C.
Go when the design has margin and the certificate is the acceptance document. A part sized off the annealed HAZ value with a generous safety factor does not need a published minimum to be safe.
No-go when the drawing requires a guaranteed tensile or yield minimum from a published table. Order 5754 for the same chemistry, or 5052 if the magnesium level is not critical.
No-go when the drawing names a marine corrosion temper. H116 and H321 are 5083 tempers under B928; there is no 5053 equivalent, so that specification has to move to 5083.
No-go above 65 °C in continuous service, and no-go for cosmetic anodizing. Both follow from the magnesium content rather than from how the metal was sourced.
No-go for high-volume machining. 5xxx alloys cut gummy and produce long chips, and 6061-T6 will be cheaper per finished part despite the higher metal price.
Specifying 5053 on the Order
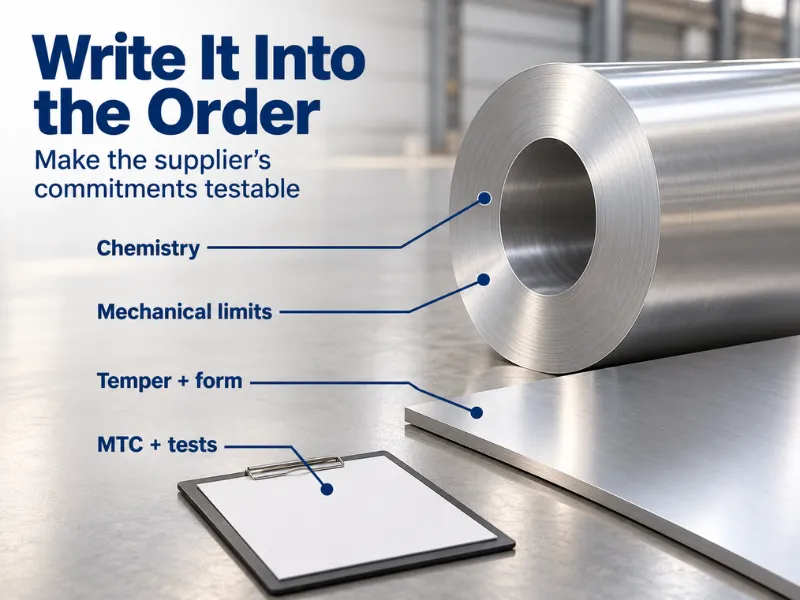
A complete line reads: 5053-H32 sheet, 1.5 mm × 1250 mm × coil, chemistry per AA register, mechanical properties on MTC. Six clauses do the work:
- Temper in H-system terms, with the mechanical values that temper is expected to deliver.
- Chemistry reference, naming the register limits so the iron and silicon lines are testable rather than assumed.
- Certificate grade. EN 10204 3.1 is the working minimum: it carries the actual analysis and mechanical results for that heat, signed within the producing works but independent of its production department. It is not a third-party document; 3.2 adds an independent countersignature if the project requires one.
- Form and dimensions, including edge condition and whether the coil is to be supplied at mill width.
- Sensitization test where the part will run warm or immersed, specified as ASTM G67 with the acceptance limit stated on the order.
- Substitution rule. State whether 5754 is acceptable in place of 5053. It usually is, it carries a standard row, and agreeing it in advance prevents a rejected delivery later.
Conclusion
5053 is a real alloy with a narrow registered chemistry and no published property minimum, which makes it a grade for drawings that already name it rather than for open selection. Its trade-off is structural: magnesium at 3.1–3.9% buys pitting resistance and weldability, and the same figure puts every heat above the 65 °C sensitization line with no B928 temper available to fix it.
We supply 5053 sheet, coil and plate to your drawing, with the heat chemistry and mechanical results on the MTC for every order, and low-MOQ custom runs in 10–60 days.
Send the temper, gauge and width, and we will confirm the rolling route and the certificate format before you commit.
Frequently Asked Questions
Is 5053 available as tread plate?
Not as a standard item. Tread and checker plate is produced in 5052, 5086 and 5754, where the tooling and the pattern rolls already exist. A 5053 pattern would be a custom pass with no published property table behind it, so specify 5754 tread plate and keep the pattern standard.
Can 5053 be used at cryogenic temperatures?
There is no qualification behind it. The 5xxx grades used at low temperature are 5083 and 5086, which carry impact-toughness data and pressure-vessel approvals down to −196 °C. Without that data, 5053 is not a defensible choice for liquefied gas containment, however well it behaves at room temperature.
Does the mill certificate still apply after welding?
Only to the unwelded parent metal. Welding anneals the heat-affected zone toward O condition, so the certified proof strength no longer describes the joint. Design the weld on annealed properties, or qualify the procedure with a weld tensile test and treat that result as the joint’s specification.
What is your minimum order for 5053, and what sizes can you roll?
We run low-MOQ custom production on 5053 in non-stock gauges and widths, typically 10–60 days depending on size and processing. Send the temper, gauge, width and coil weight and we will confirm the quantity, the rolling route and the lead time for that specification.






