


5251 aluminum is a 2% magnesium, 0.3% manganese sheet and plate alloy, registered by the Aluminum Association and specified in EN 485 and AS/NZS 1734 — but it holds no row in ASTM B209. State the applicable EN or AS/NZS standard in the order so the supplier knows which strength limits to meet.
5251 is sometimes offered instead of 5052, but it is not automatically interchangeable. Composition limits differ, and proof-strength requirements depend on the standard, temper and thickness.
What 5251 Is and Where the Standard Fixes It
5251 is a non-heat-treatable aluminum-magnesium alloy, designated EN AW-5251 and AlMg2 in the older German and ISO notation. It sits above 5005 and below 5052 in magnesium, and gains strength from magnesium in solid solution and from cold working. Composition is fixed by EN 573-3, mechanical properties for sheet, strip and plate by EN 485-2, with AS/NZS 1734 used in Australia and New Zealand. BS 1470 carried it historically and is withdrawn; ASTM B209 does not list it.
A North American drawing citing ASTM B209 5052 cannot be satisfied with 5251, and a certificate headed “5251 to ASTM B209” describes a specification that does not exist.
Chemical Composition: How 5251 Differs From 5052
The limits are EN 573-3 values, with 5052 alongside because that is the comparison buyers ask about.
| Element | 5251 (EN 573-3) | 5052 (ASTM B209) | What the number does |
|---|---|---|---|
| Mg | 1.70–2.40 | 2.2–2.8 | Sets strength and saltwater performance |
| Mn | 0.10–0.50 | 0.10 max | Refines grain, slows softening in the weld zone |
| Cr | 0.15 max | 0.15–0.35 | Controls grain growth and stress-corrosion sensitivity |
| Fe | 0.50 max | 0.40 max | Impurity; lower is better for ductility |
| Si | 0.40 max | 0.25 max | Impurity |
| Cu | 0.15 max | 0.10 max | Impurity; kept low for corrosion |
| Zn | 0.15 max | 0.10 max | Impurity |
| Ti | 0.15 max | Check other-element limits | Can act as a grain refiner |
| Others | 0.05 each / 0.15 total | 0.05 each / 0.15 total | — |
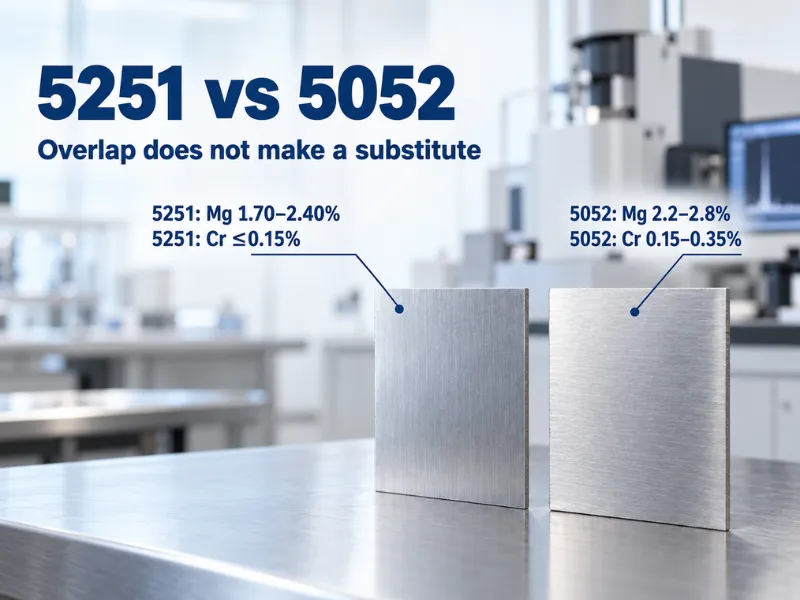
The limits differ, but are not completely separate: chromium can meet both at 0.15%, and manganese at 0.10%. This narrow overlap does not make the grades interchangeable. Any dual certification must meet all composition, mechanical and product-standard requirements.
Mechanical Properties: The 25% Gap in Proof Strength
The limits are EN 485-2 values for sheet in the 1.5–3.0 mm band, where most of this grade is bought. Single values are minima; ranges are tensile windows.
| Temper | Tensile Rm (MPa) | 0.2% proof Rp0.2 (MPa) |
|---|---|---|
| O | 160–200 | ≥60 |
| H22 | 190–230 | ≥120 |
| H24 | 210–250 | ≥140 |
| H26 | 230–270 | ≥170 |
| H32 | 190–230 | ≥120 |
| H34 | 210–250 | ≥140 |
| H36 | 230–270 | ≥170 |
| H38 | ≥255 | ≥200 |
For the H32 conditions compared here, the listed proof minima are 120 MPa for 5251 under EN 485-2 and 160 MPa for 5052 under ASTM B209. That is a 25% difference between these specified limits, not every product. A design requiring 160 MPa cannot rely on material guaranteed only to 120 MPa. Check the exact standard edition and thickness before substitution.
Do not substitute H2x for H3x without approval. H22 is strain hardened then partially annealed; H32 is strain hardened then stabilised. Matching values in this table do not make their processing identical. Both must meet the requirements of the ordered standard. Supply the temper named on the drawing.
The standard changes the acceptance limits. EN and AS/NZS requirements can differ for the same alloy and temper. A result may pass one specification and fail another. State the standard edition and thickness in the enquiry, and explicitly request the proof-strength requirement used in your design.
Forming and Temper Choice
Check elongation as well as strength when selecting a forming temper. In the same 1.5–3.0 mm band EN 485-2 guarantees ≥16% at O, ≥8% at H22 and H32, ≥6% at H24 and H34, ≥5% at H26 and H36, and ≥3% at H28 and H38.
O suits deep drawing and roll forming; H22 and H24 hold shape without hard forming; H32 is the workhorse, quarter-hard, stabilised, widest range of gauges; H34 adds 20 MPa of proof at a real cost in elongation; H36 and H38 leave little but shearing and generous-radius bending.
The bend radii below are recommendations, not guarantees; t means sheet thickness. Confirm the bend-line orientation relative to the rolling direction before using them.
| Temper | 0.4 mm | 0.8 mm | 1.6 mm | 3.2 mm |
|---|---|---|---|---|
| O | 0t | 0t | 0t | ½t |
| H32 | 0t | 0t | 1t | 1½t |
| H34 | 0t | 1t | 1½t | 2t |
| H36 | 1t | 1t | 1½t | 2½t |
| H38 | 1t | 1½t | 2½t | 3t |
Actual bend limits depend on bend-line orientation, tooling condition, die width and the supplied temper. H22 and H32 may behave differently despite similar strength values. For tight bends, test a strip of the material with the intended tooling first.
Corrosion and Service Temperature
5251 has good resistance to seawater, salt spray and atmospheric exposure. Check the actual environment before deciding whether a protective finish is needed.
High-magnesium 5xxx alloys can form magnesium-rich phases along grain boundaries during prolonged elevated-temperature exposure, reducing resistance to intergranular corrosion and stress corrosion cracking. This explains the caution around sustained service above 65 °C. With no more than 2.4% Mg, 5251 is less susceptible to this mechanism, but its allowable temperature still depends on strength, weld filler and service conditions. H116 or H321 does not remove the high-temperature risk in 5083.
For continuous immersion, compare corrosion requirements and test data before replacing specified 5083 with 5251. Magnesium content alone does not establish equivalence.
For a uniform decorative anodized finish, approve a sample first. Composition, surface condition and processing affect appearance. Consider 5005 or 1050 if the result is unsuitable.
Welding: The Filler Choice That Gets Misquoted
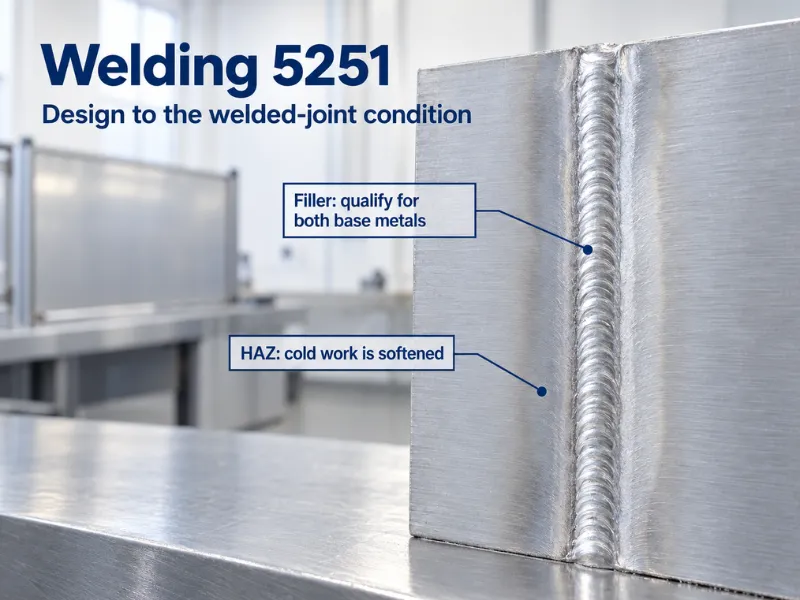
5251 welds readily by GMAW and GTAW, and the filler choice is narrower than most datasheets imply.
5356 is commonly recommended for 5251-to-5251 joints and some dissimilar-alloy joints. Confirm suitability for both base metals and the service conditions; its composition differs from 5251.
4043 may suit certain joints between 5251 and lower-magnesium or non-magnesium alloys. Do not decide by alloy family alone: check filler guidance for the exact pair of base metals and qualify the procedure. It is not automatically unsuitable merely because both parts are 5251.
Welding softens cold-worked material in the heat-affected zone, and heat treatment cannot restore that strengthening. Use the applicable welded-joint design values, not unwelded H-temper strength.
5251 vs 5052, 5754 and 5083
| Alloy Grade | 5251 | 5052 | 5754 | 5083 |
|---|---|---|---|---|
| Standard | EN 485-2, AS/NZS 1734 | ASTM B209, EN 485-2 | ASTM B209, EN 485-2 | ASTM B209, B928 |
| Mg (%) | 1.70–2.40 | 2.2–2.8 | 2.6–3.6 | 4.0–4.9 |
| Cr (%) | 0.15 max | 0.15–0.35 | 0.30 max | 0.05–0.25 |
| H32 proof minimum (MPa) | 120 (EN, conditions above) | 160 (B209, conditions above) | Check standard and thickness | Check standard and thickness |
| Marine tempers | Not applicable | Not applicable | Not applicable | H116, H321 |
| ASTM B209 row | No | Yes | Yes | Yes |
Against 5052, check the specified alloy and standard first. A drawing requiring B209 5052 cannot be met with 5251 without an approved change. Likewise, replacing specified 5251 with 5052-H32 needs approval and checks of strength, forming and corrosion requirements.
Against 5754, the magnesium ranges differ: 5251 is 1.70–2.40%, while 5754 is 2.6–3.6%. Both can suit welded sheet work, but are not automatic substitutes. Compare standard requirements at the ordered temper and thickness, then verify the supplied material against them. Any alloy change needs design and welding review.
Against 5083 there is no comparison in immersion service. Where a drawing calls for a corrosion-controlled marine temper, 5083 is the grade that has one.
Go / No-Go, and Where 5251 Is Used
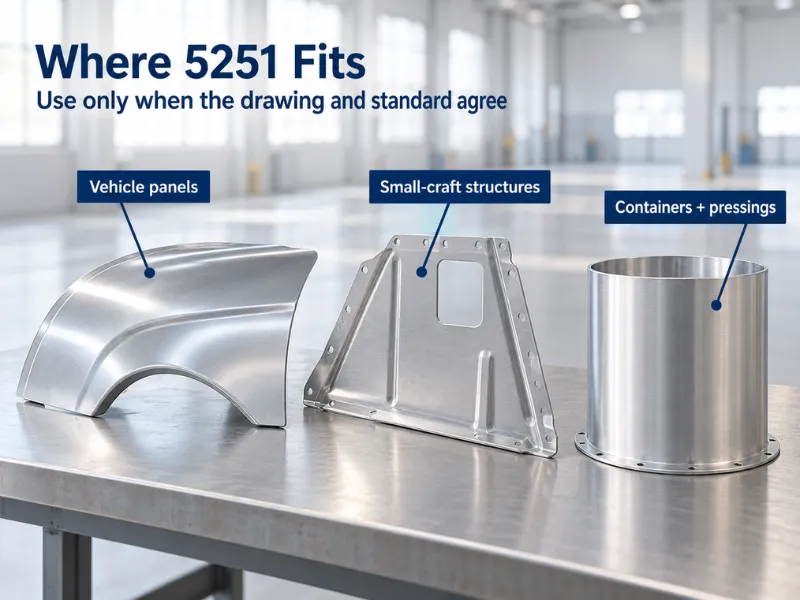
Go when 5251 meets the drawing, material standard and approved fabrication procedure. For formed or welded assemblies, check the actual load, corrosion exposure and temperature. Low magnesium reduces one sensitization risk; it does not set the assembly’s temperature rating. For prolonged hot service, review the weld filler as well as the sheet: 5356 can introduce a high-magnesium weld deposit.
No-go when 5251 is outside the specified product standard, the selected temper cannot guarantee the required proof strength, or a required marine corrosion temper is unavailable. For decorative anodizing, approve a sample before committing.
Typical applications include small-craft hulls and superstructures, vehicle panels, silos, containers and architectural pressings. At 2.69 g/cm³, it weighs about one-third as much as steel at equal volume. This weight advantage does not establish load capacity; structural parts still need design checks.
Specifying and Sourcing 5251
Include these four requirements in your order:
- Name the standard, not just the alloy. “5251-H32 to EN 485-2” leaves nothing to interpret; “5251-H32” alone allows a certificate to a standard with different limits.
- State the proof strength you need. If the design requires 160 MPa, state it and check which temper guarantees it. The H32 minimum listed here does not.
- Name the temper precisely. H22 and H32 are not interchangeable even where the table values match.
- Require EN 10204 3.1. That certificate carries the heat’s actual analysis and mechanical results, signed at the producing mill, and lets you check the metal against the limits you specified.
We roll 5251 sheet and coil in O, H22, H24, H32, H34 and H38, and cut plate to your drawing; our 5251 aluminum sheet and coil page carries the gauges and widths we run. For non-stock sizes and tempers, ask us to confirm production options and lead time, typically 10–60 days on low-MOQ runs. For bar, tube or wire, confirm the applicable product standard and required properties rather than applying sheet values.
Conclusion
5251 and 5052 have different composition limits and cannot be treated as automatic substitutes. Their guaranteed strength also depends on standard, temper and thickness. Specify 5251 under an applicable product standard, check forming and service requirements, and obtain approval for substitutions. Its low magnesium content reduces high-magnesium sensitization risk, but does not remove temperature or welding checks.
We supply 5251 to the applicable standard agreed for your order, with the temper and proof minimum written onto the order and a 3.1 certificate carrying that heat’s actual results.
Send your drawing with the standard number, temper and required proof strength, and we will confirm whether 5251 is the right answer or whether 5754 gets you there with less paperwork.
Frequently Asked Questions
Is 5251 the same as 5052?
No. The composition limits differ, although they overlap at the chromium and manganese boundaries. Matching chemistry alone does not establish equivalence. Check the specified standard, temper, thickness and mechanical requirements before substitution.
Why is 5251 not in ASTM B209?
Product standards list selected alloys and tempers; registration alone does not ensure inclusion. 5251 is specified in EN 485 and AS/NZS 1734 rather than B209. If B209 is required, assess a covered alloy such as 5052 or 5754 and obtain substitution approval.
What filler wire should I use for 5251?
5356 is a common option. Depending on both base metals and service requirements, 4043 may also be suitable. Check filler guidance for the exact joint and confirm the choice through procedure qualification, especially for dissimilar alloys or elevated-temperature service.
What is the lead time and minimum order for 5251 sheet?
Low-MOQ custom runs are available; stock gauges move faster. Typical lead time is 10–60 days depending on gauge, width and temper, and every order ships with an MTC.






