What Is 6010 Aluminum?
6010 is a heat-treatable aluminum-magnesium-silicon alloy of the 6xxx family, with copper present as a deliberate addition. It was developed in the United States in the mid-1970s as an automotive body-sheet grade.
Its defining feature is not peak strength. It is the combination of formability in the T4 condition with a measurable strength increase during the paint-bake cycle. A stamped panel arrives soft enough to deep-draw, then hardens in the same oven that cures the paint.
That is why the later body-sheet alloys — 6016 in Europe, 6111 and 6022 in North America — were tuned for a stronger bake-hardening response and better formability. 6010 stays in service for parts where the drawing already names it; if the design is still open, one of those grades is the current default.
Chemical Composition of 6010
The limits below are the registered ranges, which agree across the Aluminum Association registration, EN 573-3, and GB/T 3190.
| Element | Weight % |
| Silicon (Si) | 0.8 – 1.2 |
| Iron (Fe) | 0.50 max |
| Copper (Cu) | 0.15 – 0.6 |
| Manganese (Mn) | 0.20 – 0.8 |
| Magnesium (Mg) | 0.6 – 1.0 |
| Chromium (Cr) | 0.10 max |
| Zinc (Zn) | 0.25 max |
| Titanium (Ti) | 0.10 max |
| Others, each / total | 0.05 / 0.15 |
| Aluminum (Al) | Balance |
How to tell 6010 from 6013. The copper row is the tell. 6010 caps copper at 0.6%, while 6013 carries 0.6 – 1.1% — roughly double — with a higher magnesium range at 0.8 – 1.2%. Any table showing a copper range that starts at 0.6 and climbs is describing 6013, whatever the heading says.
The distinction is not academic. Copper drives both the aging response and the corrosion penalty, so a buyer who specs 6010 against a 6013 data sheet gets the strength and the corrosion behavior wrong in opposite directions.
If a quotation or a certificate gives composition outside the ranges above, ask which standard it was drawn from before accepting it.
Mechanical Properties by Temper
6010 does not carry the broad, consistently tabulated property record that 6061 does. Published figures vary by source and by product form, so the table below gives indicative commercial values rather than specification minimums.
| Temper | Tensile strength (MPa) | Yield strength (MPa) | Elongation (%) |
| O (annealed) | 150 – 200 | 70 – 100 | 18 – 22 |
| T4 (solution treated, naturally aged) | 250 – 310 | 130 – 180 | 20 – 24 |
| T6 (artificially aged) | 290 – 340 | 240 – 290 | 10 – 14 |
T4 is the condition this alloy is built around. It is the state in which 6010 is formed, and the state in which most of it reaches automotive customers.
Two cautions before you use these numbers.
First, the spread is wide enough to matter. Reported 6010-T4 tensile strength appears at 255 MPa in one engineering reference and near 290 MPa in another, for the same designation. Do not design from a midpoint.
Second, the T6 figures are typical values, not guaranteed minimums. For any loaded part, require the mechanical results on the mill test certificate for the ordered form and thickness.
On T651. 6010 is a sheet and coil grade, and T651 — T6 with residual stress relieved by stretching — is not a standard supply condition for it. No common commercial listing of the alloy includes it, so a drawing calling for 6010-T651 needs availability confirmed before quoting. For a formed panel, T4 is almost always the condition actually wanted.
Physical Properties
| Property | Value |
| Density | ~2.70 g/cm³ |
| Melting range | ~580 – 650 °C |
| Coefficient of thermal expansion | ~23.6 × 10⁻⁶ /°C (20–100 °C) |
| Modulus of elasticity | ~69 GPa |
| Thermal conductivity | Commonly quoted near 200 W/m·K; not a tabulated value in a product standard |
| Electrical conductivity | Commonly quoted above 50% IACS in the annealed condition; verify per lot |
The last two rows deserve a sentence rather than a bare number, because they are the rows most often copied from the wrong alloy.
6010’s alloying level sits close to 6061’s: slightly more silicon, a similar magnesium range, and a copper ceiling only marginally higher. On that basis there is no reason to expect 6010 to be a markedly better or worse conductor than 6061, and figures quoted in the 200 W/m·K range are consistent with that. Those figures are not a design value, though — thermal and electrical conductivity are not listed in a sheet product standard, so any heat-transfer calculation needs a measured number on the mill datasheet.
The expansion row is there for completeness only. Every 6xxx alloy sits within a rounding error of the others on thermal expansion, so this is not a property that should decide a material selection.
6010 vs 6061 vs 6063
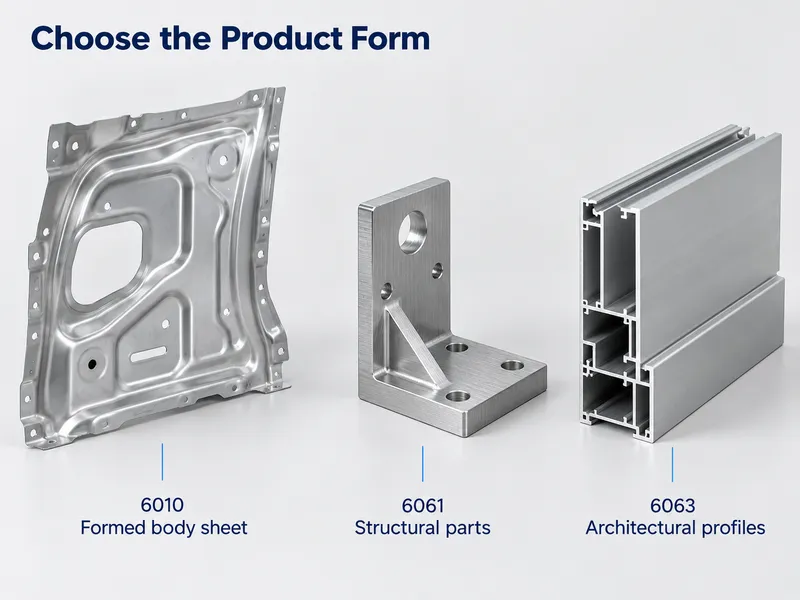
The comparison is aligned at T6, the temper all three are commonly specified in.
| Alloy | Principal alloying | Tensile strength (T6) | Corrosion resistance | Weldability | Typical use |
| 6010 | Mg 0.6–1.0, Si 0.8–1.2, Cu 0.15–0.6 | 290 – 340 MPa | Good, but not above 6061 | Weldable; HAZ softens | Automotive body sheet, formed panels, welded assemblies |
| 6061 | Mg 0.8–1.2, Si 0.4–0.8, Cu 0.15–0.40 | ~310 MPa | Very good | Excellent | General structural work, marine frames, machined parts |
| 6063 | Mg 0.45–0.9, Si 0.2–0.6 | ~240 MPa | Very good | Excellent | Architectural extrusions, window systems, heat sinks |
Read the tensile row first: 6010 and 6061 land in the same band, and 6063 sits clearly below both. So 6010 is not a strength upgrade over 6061 — it is a forming and bake-hardening grade that happens to reach a similar aged strength, and it does so while giving up corrosion margin to copper.
The last two rows are what separate the three. 6063 leads on extrudability and surface finish, which is why it takes the architectural and thermal work, while 6061 takes the structural work with the same strength as 6010, better corrosion behavior, and a far deeper body of published data. 6010’s claim is the form-then-bake route, and it is worth choosing only where that route is the point.
What the Copper Content Changes
Copper in this alloy does four things, and they do not all point the same way.
Strength — positive. Copper joins the magnesium-silicide precipitation and raises the aged strength. That is why 6010 reaches 6061’s level despite carrying less magnesium.
Corrosion resistance — negative. Copper sits in the aluminum matrix as cathodic intermetallic particles, and those particles raise the risk of pitting and intergranular attack. 6010 permits copper up to 0.6% against 6061’s 0.40% ceiling, so 6010 should not be assumed to be the more corrosion-resistant of the two. Where a part will sit unpainted, wet, or in salt exposure, 6061 is the safer starting point.
Weldability — qualified, not assumed. Standard Al-Mg-Si filler practice transfers from 6061, but a procedure qualified on 6061 should be re-qualified rather than carried over.
Finishing — cosmetic risk. Copper-bearing alloys can anodize to a slightly warmer or less uniform tone than low-copper grades. Where color consistency is a specification line, run a sample through the actual finishing line first.
The claim worth discarding is the one that circulates most widely about this alloy: that 6010 resists corrosion better than 6061 because it contains more magnesium and silicon. 6010’s corrosion story is a genuine improvement — but an improvement over the 2xxx body-sheet grades it replaced, not over 6061.
Working With 6010
Forming. T4 is the forming condition and where the alloy performs best, with good cold formability and a sharp drop in T6. If a part needs maximum ductility before any aging, O is the forming stock, with the temper applied afterwards.
Bake hardening. This is the commercial reason the alloy exists. A panel is formed in T4 and reaches service strength through the paint-bake cycle rather than a separate aging step. If you specify 6010 and then skip the bake, you are not getting the properties the grade was chosen for.
Welding. MIG and TIG both work, using standard Al-Mg-Si filler logic: ER4043 where crack resistance and puddle control dominate, ER5356 where higher weld strength or a better anodizing color match matters.
The heat-affected zone is the part that gets underestimated. 6010 is a heat-treatable alloy, and fusion welding overages or dissolves the strengthening precipitate in the HAZ, cutting local strength by as much as half. Size the joint on reduced HAZ values — the weld-condition allowable in AWS D1.2, or the equivalent European reduction — not on T6 parent properties.
Post-weld aging recovers only a small fraction of that loss. Full recovery would mean re-solution treating and quenching the finished assembly, and the quench distortion normally rules that out.
Machining. The aged tempers machine well and produce shorter chips than T4, which tends to be gummier. Standard aluminum tooling and cutting fluids apply.
Finishing. 6010 anodizes acceptably, though the copper content can leave a slightly warmer tone than low-copper grades. For visible parts, confirm the finish on a sample rather than from a specification sheet.
Where 6010 Is Used
| Sector | Application |
| Automotive | Outer and inner body panels, structural sheet components, brackets |
| Transport equipment | Trailer and container bodies, side panels, flooring sheet |
| Welded fabrication | Assemblies and brackets where forming and welding are both required |
| General sheet work | Formed parts that are painted or coated after fabrication |
Do not file this alloy under “aerospace.” 6010 is a body-sheet grade, not an aerospace structural alloy. Where a modern automotive program selects a 6xxx body sheet today it will normally name 6016, 6111, or 6022 — 6010 appears when an existing drawing or a legacy assembly already specifies it.
Go/No-Go: When to Specify 6010
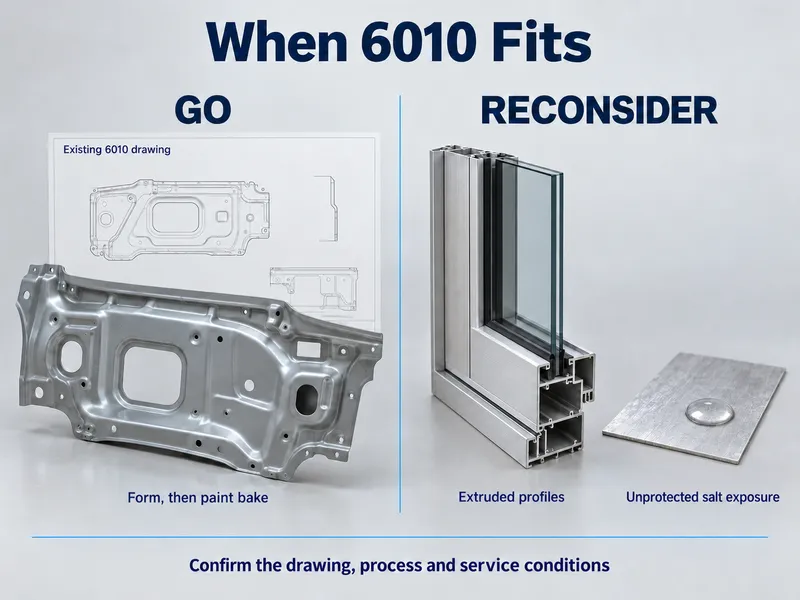
Go — specify 6010 when:
- An existing drawing, platform, or customer assembly already names 6010, and substitution is not on the table.
- The process route is form-then-paint-bake, and the part gains its strength in the coating oven.
- The part is formed from sheet or coil and welded into an assembly, with HAZ knockdown accounted for in the design.
- The service environment is painted or otherwise protected, so the copper penalty is contained.
No-go — choose something else when:
- The part sees unpainted marine, coastal, or de-icing salt exposure — 6061, or a marine 5xxx grade such as 5083.
- You need a step up in strength rather than a forming grade — 6061, 6082, or a 7xxx alloy, depending on how much.
- The form is an extrusion or a profile rather than sheet — 6063 for finish and extrudability, 6061 where structure matters.
- The application is heat transfer — 6063 is the better 6xxx choice, at around 201 W/m·K typical for T6.
- You need a current body-sheet specification with well-documented bake-hardening data — 6016, 6111, or 6022.
Sourcing 6010 Sheet, Plate, and Coil
6010 is a specialist automotive-body grade, so the sourcing questions that matter are narrower than they are for 6061.
- Forms. Sheet, plate and coil are the standard range. Tube, bar and extruded profile sit outside it and are produced to drawing on a low-MOQ basis.
- Temper. T4 is the routine condition, and T6 is available where a non-formed part needs full aged strength. Treat T651 as a special inquiry, not a catalog item.
- Documentation. A mill test certificate carrying actual chemical analysis and mechanical results per lot is the baseline. Third-party inspection is arranged on request where a project calls for it.
- Lead time. On a custom item, allow roughly 10 – 60 days depending on alloy, dimensions, and processing requirements. Stock sizes move faster.
What to put in the inquiry: the temper, the thickness range, whether the part will be formed and paint-baked, and whether the assembly is welded. Those four answers change what the mill should supply, and they are the reason a generic 6010 quote is rarely the right one.
Thin grades like this are where stock breadth and low-MOQ custom production matter more than headline capacity — we hold and cut 6010 sheet and plate as part of our 1000–8000 series range, so a small or mixed-spec order does not have to wait on a full mill run.
Conclusion
6010 is a copper-bearing 6xxx body-sheet alloy whose value is specific: it forms in T4 and reaches service strength through paint bake, and it is not a strength upgrade over 6061. The trade-off is that it is a legacy grade — supply is narrower than for 6061, the published property record is thin and widely copied from the wrong alloy, and the copper that raises its aged strength also lowers its corrosion margin.
We supply 6010 sheet, plate, and coil in T4 and T6, cut to your dimensions at low minimum order quantities, with an MTC reporting actual chemistry and mechanical results on every order.
Send us your drawing, temper, and thickness range for a grade-fit check.
Frequently Asked Questions
What is the lead time and minimum order for 6010 sheet?
Custom production typically runs 10–60 days, depending on alloy, dimensions and processing. Stock sizes ship far sooner where they are held. Treat 6010 as a made-to-order grade and plan the schedule around it.
What documents come with a 6010 order?
An MTC reporting the actual chemical analysis and mechanical results for the lot, issued with every order. Third-party inspection can be arranged on request for projects that call for it, so agree the requirement at enquiry stage rather than after the order.
Can 6010 be substituted for 6016 or 6111?
Not without a re-qualification. All three are 6xxx body-sheet grades, but 6010 is the legacy member with a much thinner published property record and different copper and magnesium limits. Where a current programme specifies 6016, 6111 or 6022, quote against that specification instead.